Get in touch with Shengtu Bufan Company
Freeze-Drying & Drying Equipment
Freeze Dryer Manufacturers for Food Plants: Two Drying Routes, One Supplier
Most freeze dryer manufacturers reachable from a search result build for home kitchens or laboratory benches. Shengtu builds neither. We build two production routes for food plants — vacuum freeze drying and continuous mesh-belt hot-air drying — and this page exists to tell you which one your product belongs on before anyone quotes you a machine.
- Belt route: engineered quotation within 24 hours
- Belt route builds in 30–40 working days from drawing approval, freeze dryers in 60–120 working days from the deposit clearing
- Minimum order is one machine
- Installation and commissioning by our own engineers
Send Your Product Brief for a Quote
Send the product, the throughput and the two moisture numbers. An engineer reads it before any figure is issued.
Get a Quote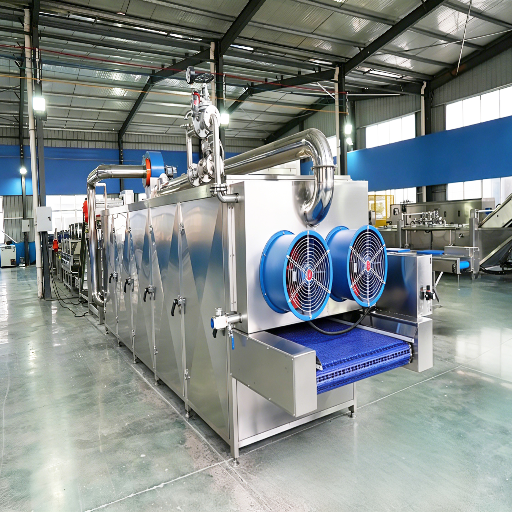
Quotation Turnaround
Within 24 hours, with an equipment proposal, a layout suggestion and an energy estimate
Lead Time
30–40 working days for one standard machine, 30–60 working days for a customized or line-integrated dryer, counted from drawing approval
Payment Terms
30% deposit, balance before shipment, by bank transfer
Warranty
Warranty duration, coverage and exclusions are confirmed in the quotation and contract
Lead Time
60–120 working days from the date the deposit clears
Payment Terms
Telegraphic transfer against a deposit at order confirmation, or a letter of credit
Warranty
Warranty duration, coverage and exclusions are confirmed in the quotation and contract
Minimum Order
One machine
Installation
Our engineers travel to your site to direct installation, complete commissioning and train your operators
Food Drying Equipment: Two Routes This Category Covers
A freeze dryer manufacturer for food production is a builder of vacuum sublimation plant sized to a customer’s daily water-removal load, not to a catalog model number. That is the definition this page works to, and it is why the two machine families below are quoted from your product data instead of from a price list. Both routes are preservation processes that pull water out until the product is stable at ambient temperature; they differ in how they take it out.
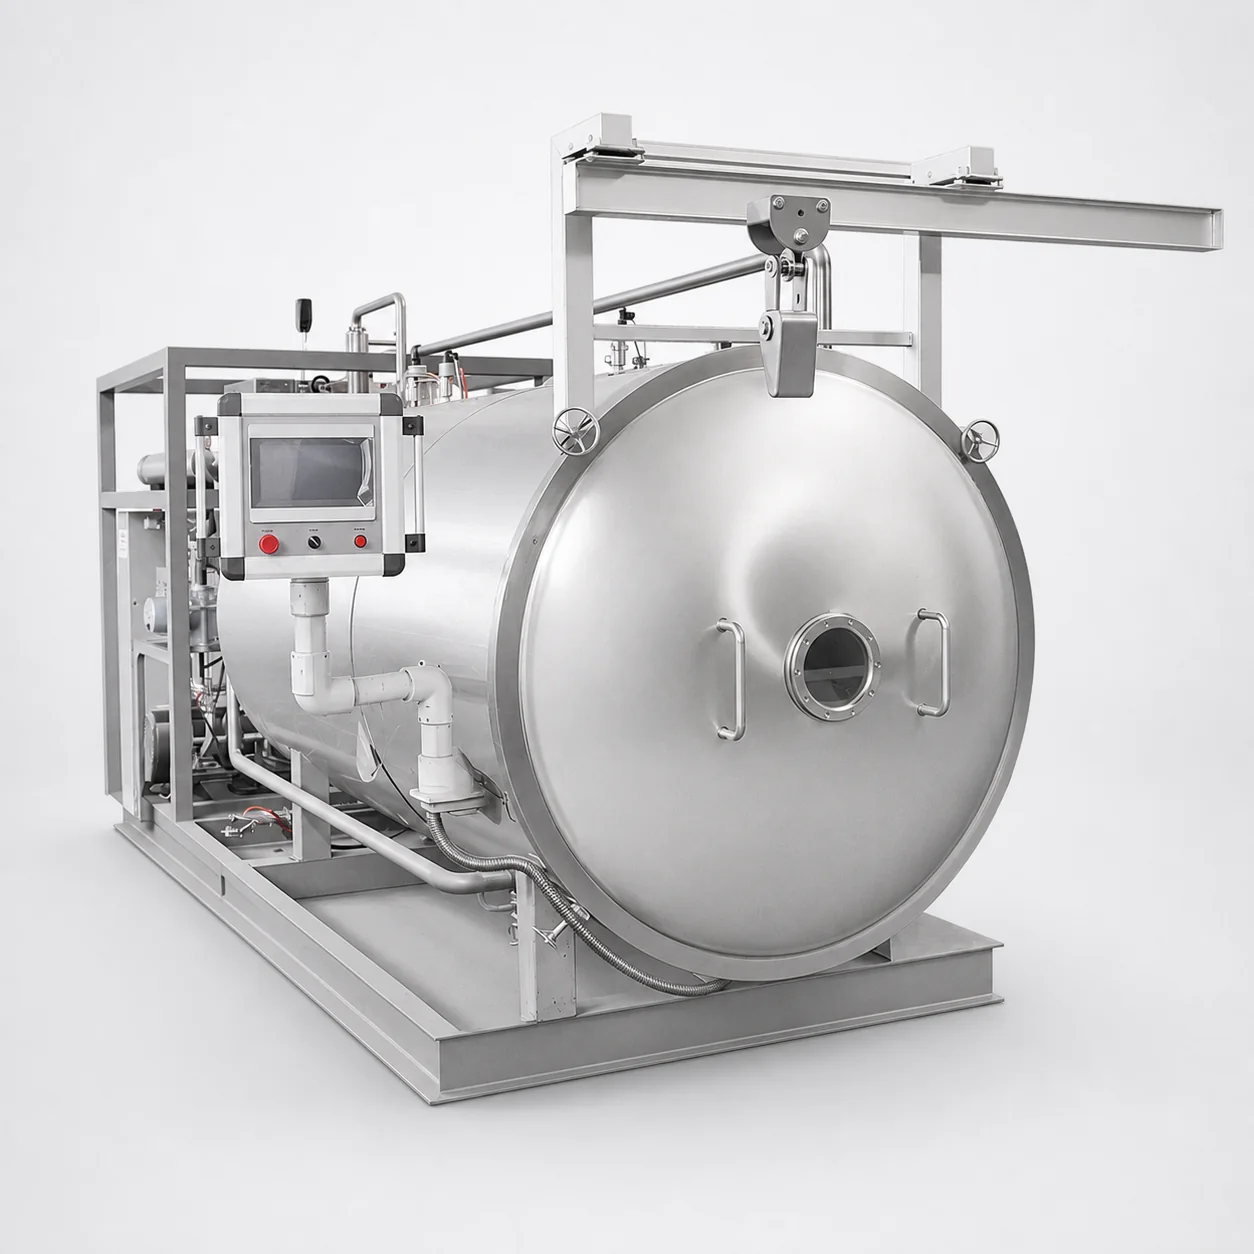
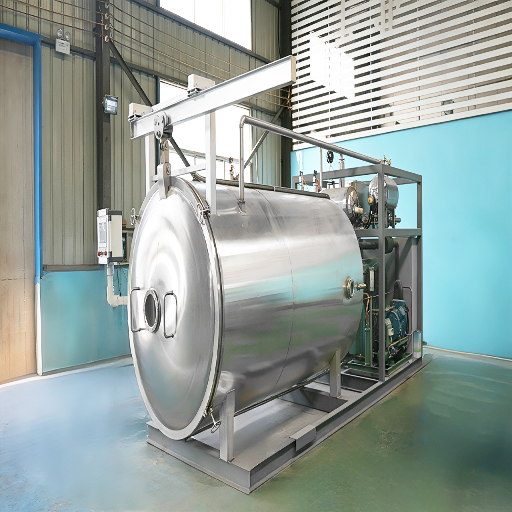
Vacuum freeze drying
The product is frozen solid, the chamber is pumped below the triple-point pressure of water, and shelf heat drives ice straight to vapor without passing through a liquid stage. The vapor re-freezes on a cold condenser instead of passing through the vacuum pump.
- Four stages: freezing, vacuum draw-down, primary drying, secondary drying
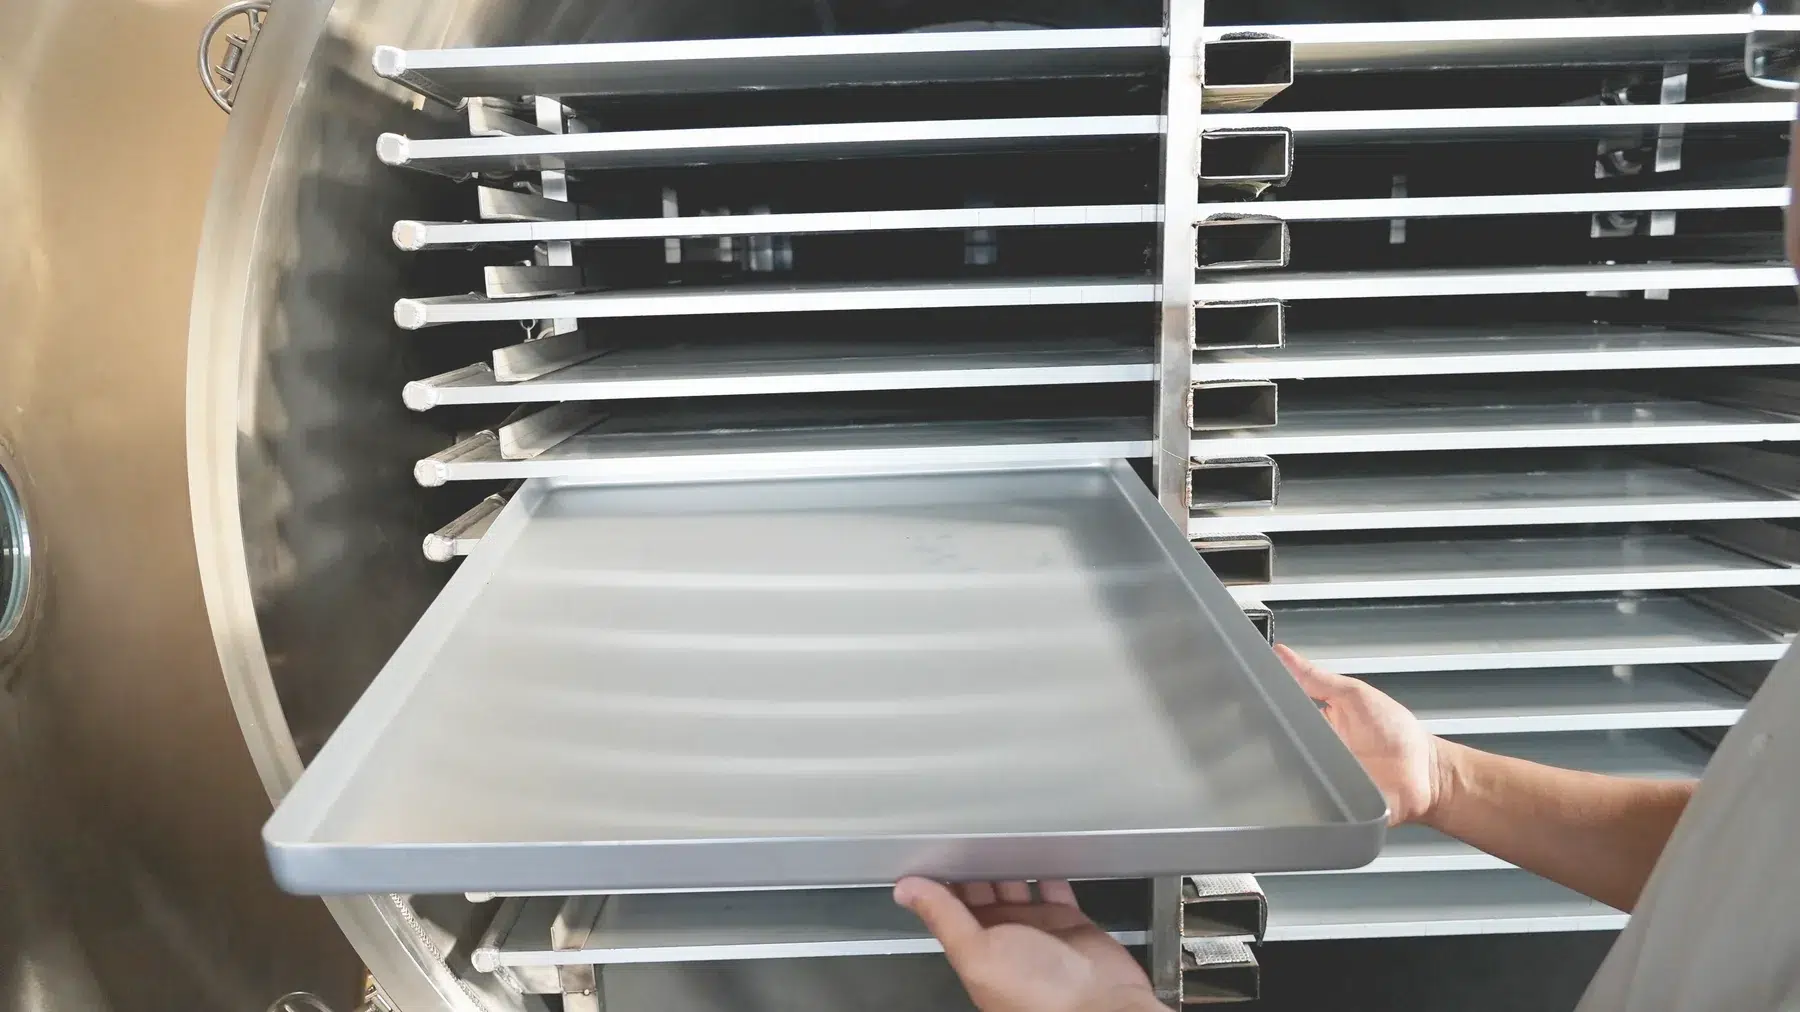
- Batch process — trays on trolleys, one recipe per chamber load
- Reaches the lowest residual moisture of the two routes
- Holds piece shape, color and cell structure through the cycle
Vacuum Freeze Dryer — full specification and sizing method
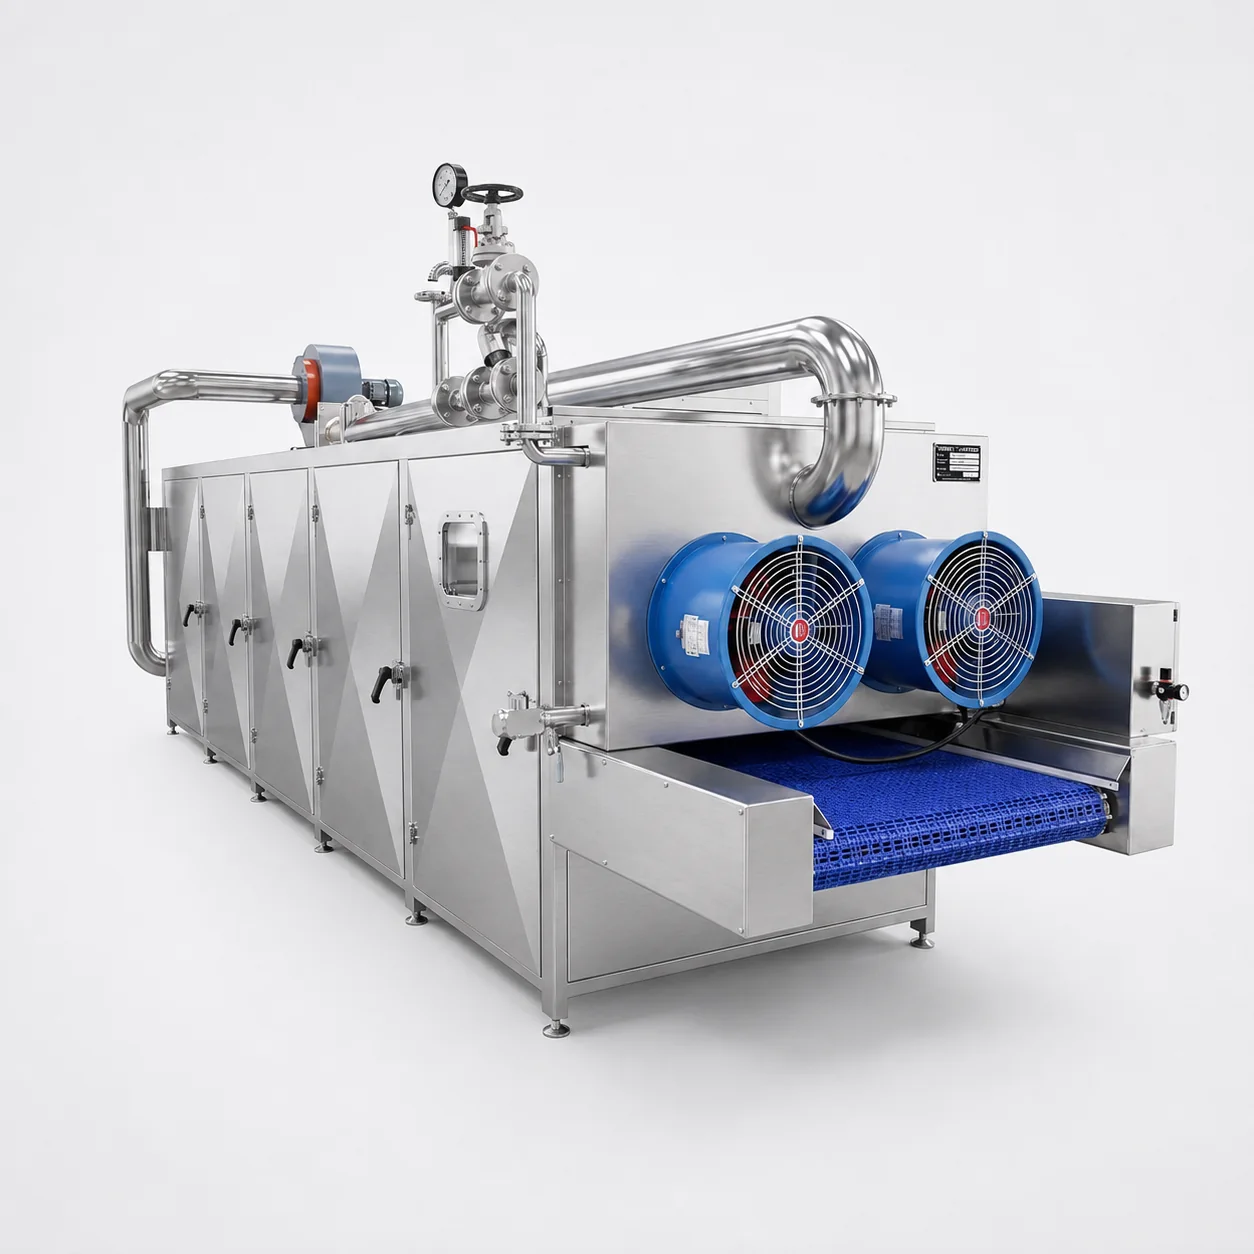
Continuous mesh-belt hot-air drying
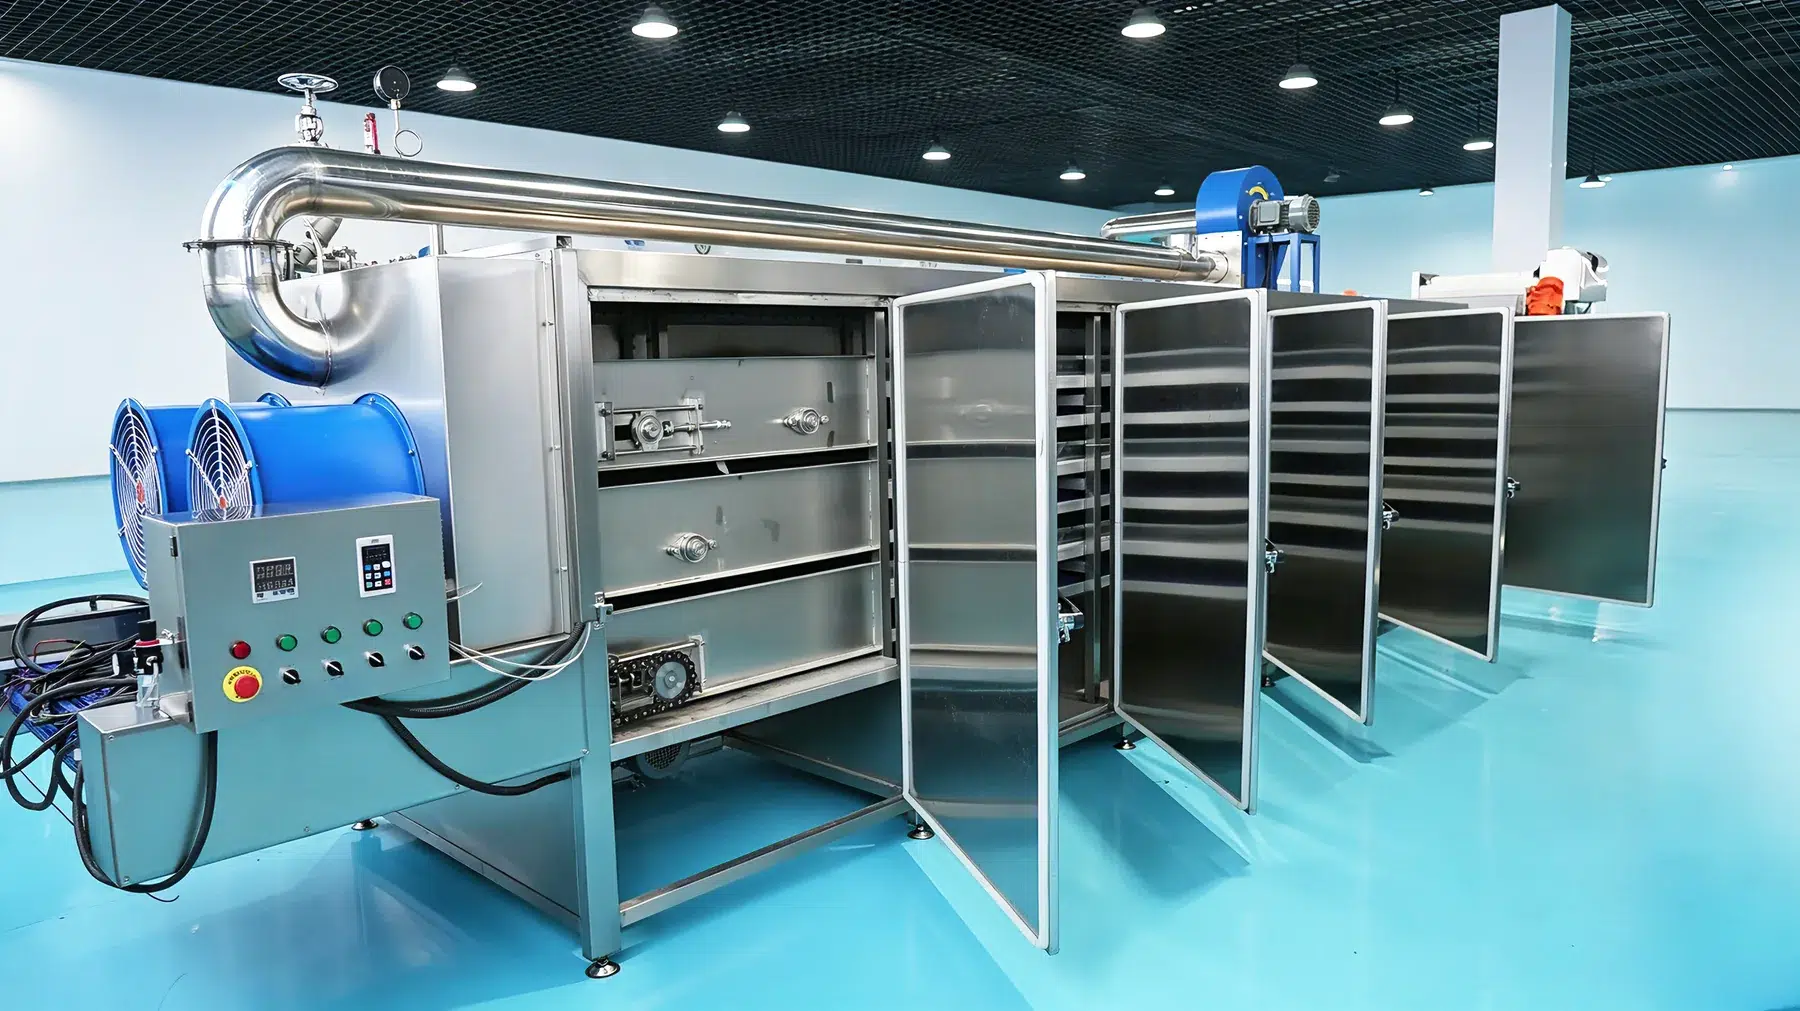
Wet product travels through an enclosed tunnel on a perforated stainless belt while heated air is forced through the bed rather than across it. Humid air is exhausted and dried product discharges continuously at the far end.
- Enclosed tunnel divided into independently controlled heating zones
- Continuous process — product enters and leaves without the machine stopping
- Single-layer or multi-layer belts, stacked to multiply drying area inside one footprint
- Built as a conveyor belt dryer for line integration, or as a standalone continuous belt dryer
- Steam, electric, natural gas or heat-pump heating
- Heat-source hardware is built in-house, except a sourced burner on the natural-gas option and a sourced refrigeration package on the heat-pump option
Mesh-Belt Hot-Air Dryer — full specification and fit test
“Buyers arrive asking how many kilograms a chamber holds. We answer with a different number: how many hours one load takes, because that is what decides how many loads a year the machine will ever run. Vacuum freeze dryers offer the lowest residual moisture we can reach, and they charge for it in cycle time.”
Product families these two routes are built for
Fruit slices, dice, purée and whole berries
Vegetable dice, leafy vegetables, herbs and blanched pieces
Meat, poultry and seafood pieces, jerky strips and pet treats
Instant coffee, tea and extract slab or granulate
Probiotics, enzymes and other functional ingredients
Grain, nuts, noodle strands and coated or extruded snack pieces
Seafood work that industrial dehydration equipment is usually bought for, including shrimp, small dried fish and squid shreds
The Drying Route Crossover
The Drying Route Crossover is the line at which the extra cost of freezing and sublimating stops being repaid by what the finished product sells for. Plants that sit on the wrong side of it rarely fail loudly, and the reason is structural: a machine sized for the wrong route still runs, it just never repays itself, which is why Shengtu engineers the route decision before the machine.
It runs between these two machine families only, so the wider field of industrial drying sits outside our scope and those technologies are named in When Neither Route Is the Right Answer.
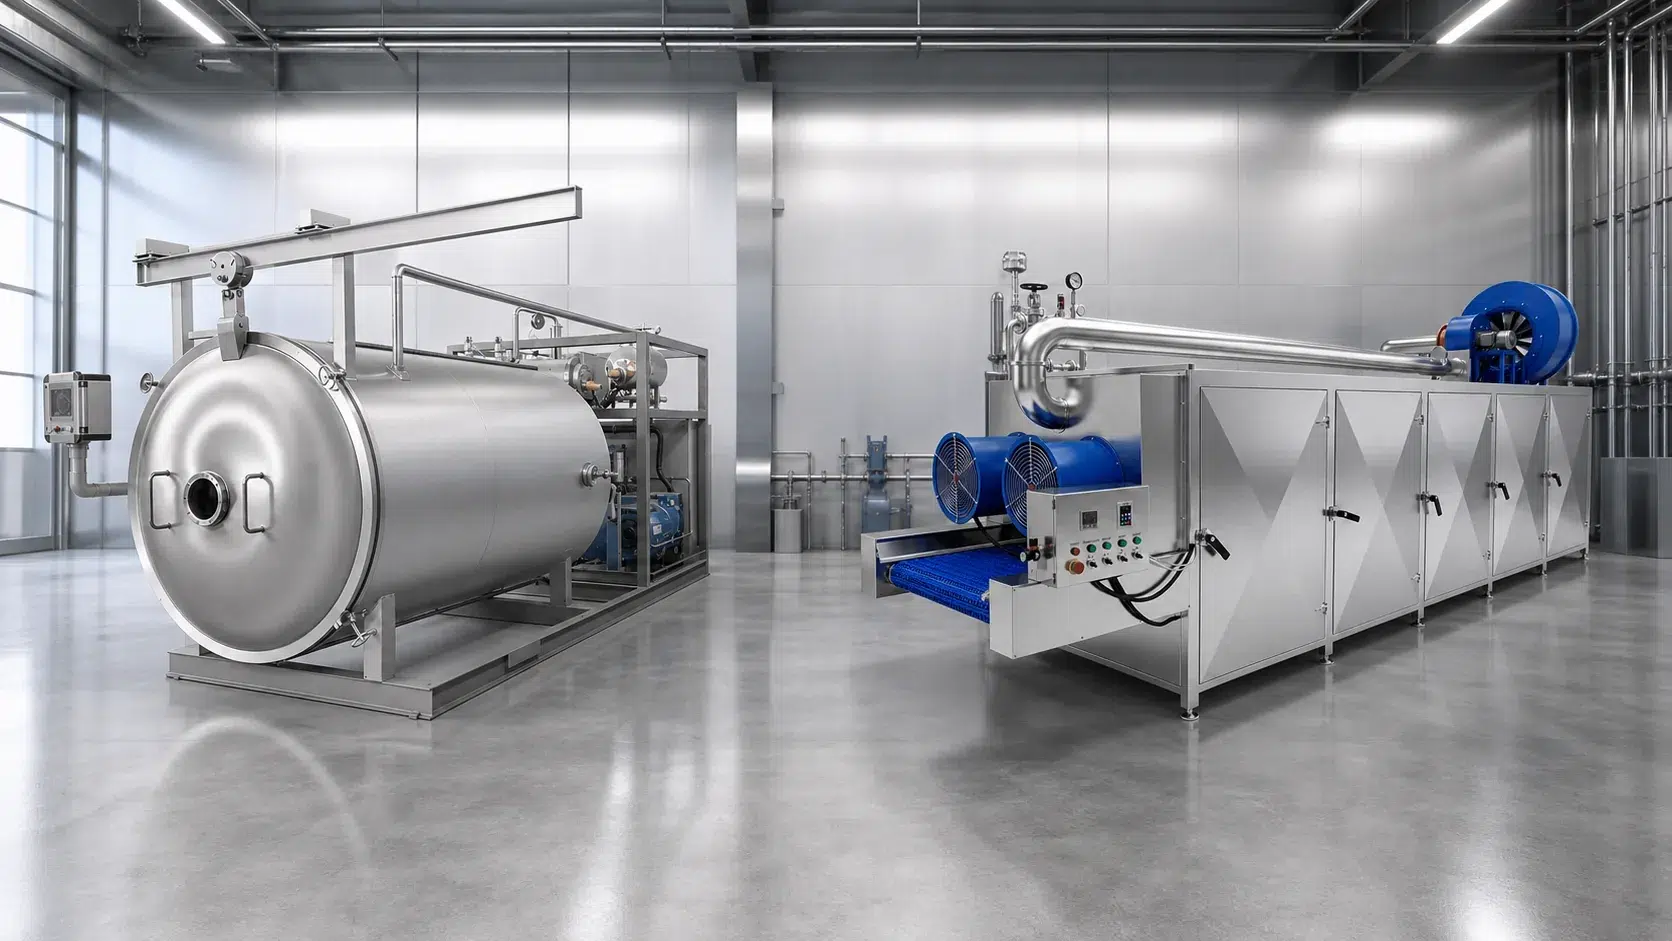
Six axes that decide the route, plus the load that sizes it
| Axis | Points to freeze drying | Points to mesh-belt hot air | Why the axis exists |
|---|---|---|---|
| Selling price of the finished product | Premium grade, ingredient sold on structure or aroma | Commodity dried product sold on price | A large class of products exists for which freeze drying is not economically justified.[2] |
| Heat sensitivity | Actives, volatile aromatics, cultures and enzymes | Product that tolerates continuous air at 50–95 °C (122–203 °F) | The belt route’s temperature band is fixed by the machine; the freeze-drying route works below it. |
| Target water activity | Ambient-stable at a low water activity target | Conventional dehydration to a storage-stable water content | Water activity, not moisture percentage, is the condition US regulation names alongside temperature and pH among those that control microbial growth.[3] |
| Rehydration and structure | Piece must return close to its original shape | Finished texture is the sold texture | Freeze drying preserves porosity; hot air shrinks and case-hardens. |
| Incoming water load sizes the machine; does not by itself pick the route |
Any, but every point of it is paid for in cycle hours | High load spread over a long multi-layer tunnel | Raw high-moisture produce carries 80 to 95 percent water,[4] and removing it is the whole job. Muscle foods sit lower — USDA publishes 56 to 73 percent across common raw beef and poultry cuts, against roughly 75 percent for lean muscle itself — and grain or nuts change the arithmetic again. |
| Continuity of production | Batch scheduling is acceptable | Line must not stop between loads | Freeze-drying condensers must be defrosted between batches; patented work exists specifically to take defrosting off the critical path.[5] |
| Composition | Lean protein and starch pieces | Lower-value high-sugar and high-fat product | High sugar lowers the collapse temperature, so shelf heat has to be fed more slowly and the cycle stretches. |
Freeze drying is always higher quality
Peer-reviewed work is explicit that one set of freeze-drying parameters cannot be used for all types of food, and that raising shelf temperature can defrost the product and collapse its structure.[6] Quality is a function of the cycle you run, not of the badge on the machine.
Nutrient retention settles the choice
Convective drying has been measured cutting vitamin C, carotenoid and phenolic content of fruits and vegetables by up to 70 percent depending on the process parameters chosen — and that same study concludes micronutrient concentration should not by itself decide the drying method, since drying time, energy use, color, texture and rehydration may matter more.[7]
A bigger chamber fixes the economics
Annual output on the freeze-drying route is set by cycle time, not by chamber volume. Two plants buying the same chamber end up with very different yearly figures because their products dry at different rates.
Machines in This Freeze Dryer and Dryer Category
Two machine families sit under this category, each with its own specification page, its own commercial terms and its own sizing method. Both are built to order against your product data.
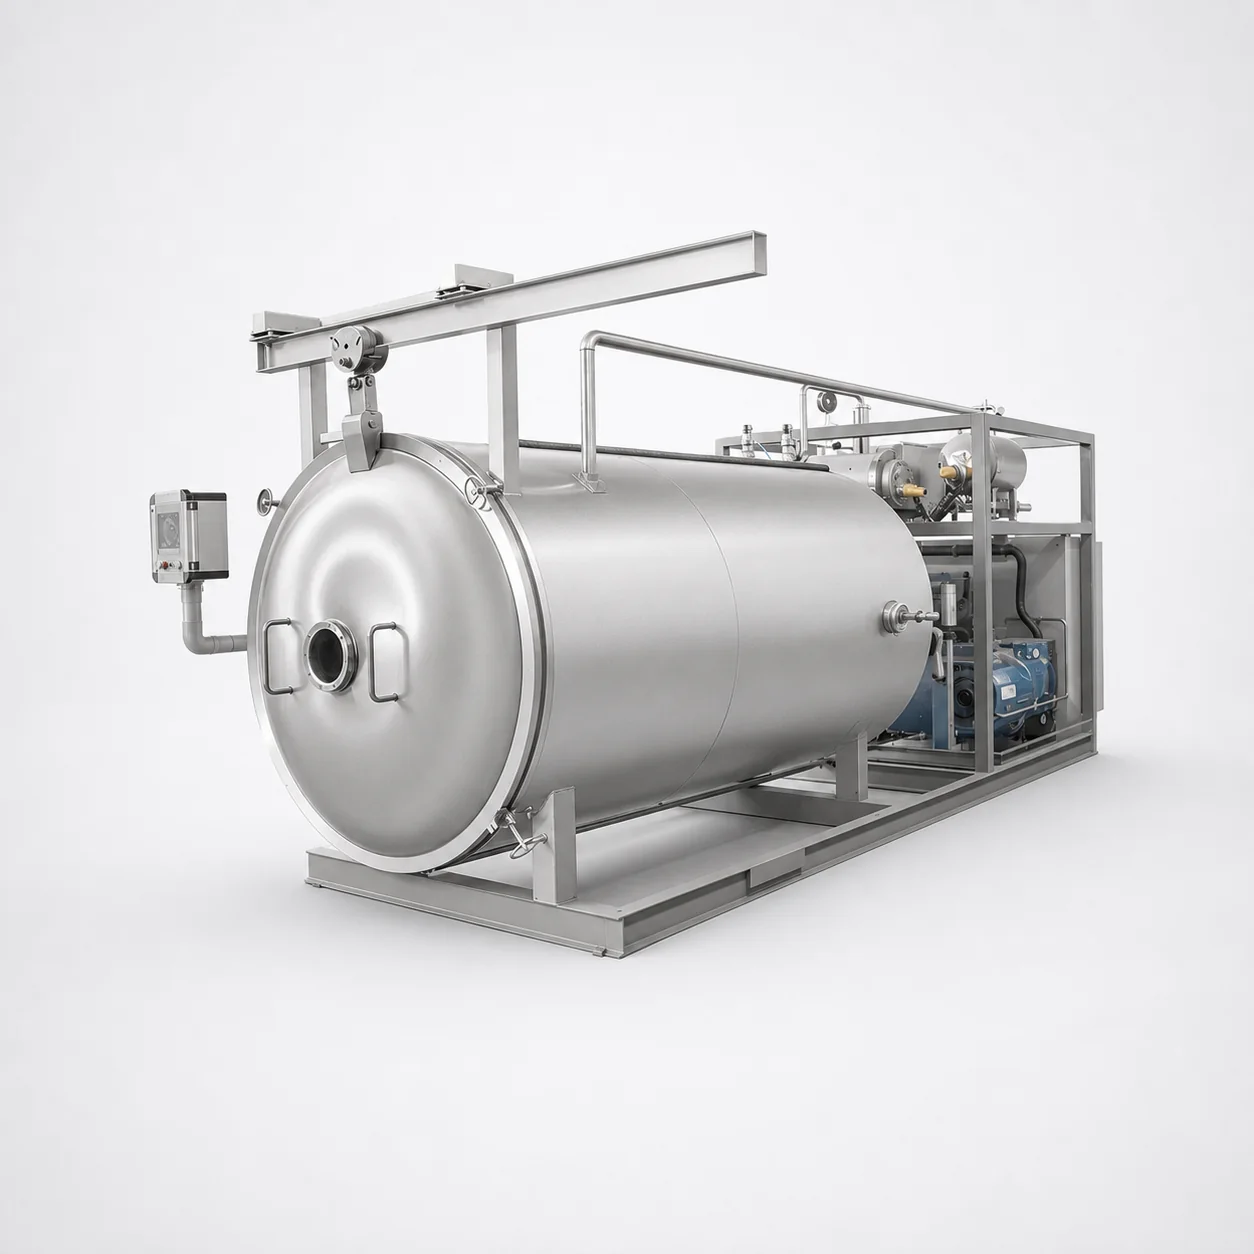
Vacuum Freeze Dryer
ProcessBatch vacuum sublimation, four stages, trolley-loaded trays
Best fitPremium fruit, coffee and tea extract, pet treats, probiotics and enzymes
Sized fromDaily water-removal load, shelf area and condenser duty — not tray area
Heating optionsElectric shelf heating, or steam and thermal-fluid heating
Defrost optionsSingle water defrost, steam defrost, or alternating automatic defrost
Lead time60–120 working days from the date the deposit clears
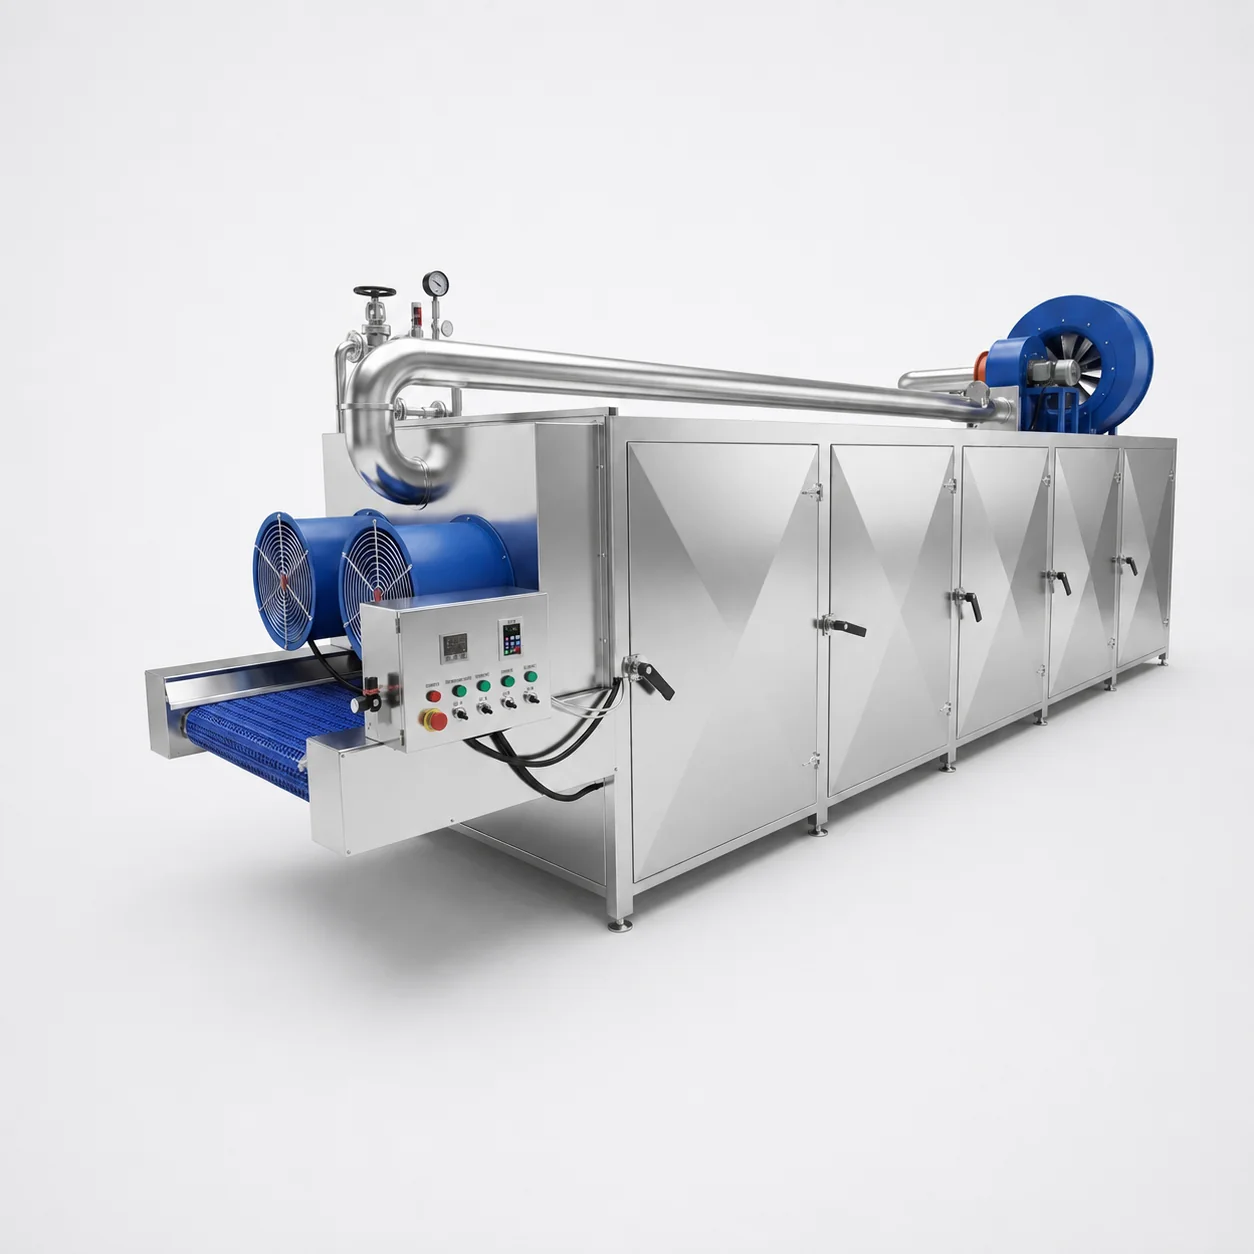
Mesh-Belt Hot-Air Dryer
ProcessContinuous through-circulation hot air on a perforated belt, zoned tunnel
Best fitVegetable slices, jerky and pet strips, seafood, tea and botanicals, grain and nuts
Sized fromHourly evaporation duty derived from throughput and the two moisture figures
Heating optionsSteam on the reference build; electric, natural gas or heat pump selectable
Belt optionsSingle-layer or multi-layer; stainless mesh or polyurethane
Lead time30–40 working days for one standard machine
Where these machines sit in a finished production line
Neither machine is bought on its own very often. Both are stations inside a line, and the stations either side of them decide whether the dryer ever reaches its rated duty.
Fruit and vegetable
Washing and cutting upstream, then either the fruit and vegetable freeze-drying line or the dehydration line.
Pet food
Raw medallion and organ work runs on the freeze-dried pet treat line; strip products run on the pet jerky drying line.
Finished dry goods
Where the freeze-dried food is itself the sold item, the freeze-dried and quick-frozen food category covers the whole-line scope.
Your product is not on this list
Send the product name with your inlet and outlet moisture targets and your throughput. We will confirm in the quotation which route it belongs in and which configuration fits.
Get a QuotePublished Specifications by Route
What each route publishes is itself a reading of The Drying Route Crossover: the two sides of that line do not carry the same kind of number. The difference below is deliberate rather than an omission. A belt dryer has a reference configuration that can be printed; a freeze dryer is sized from your water load, so a model table would be a guess dressed as a specification.
Mesh-belt hot-air dryer — reference configuration
Vacuum freeze dryer — the variables your configuration is built from
Every figure on a freeze dryer follows from your product. These are the variables an engineer fixes before a configuration sheet is issued, and none of them can be answered from a catalog.
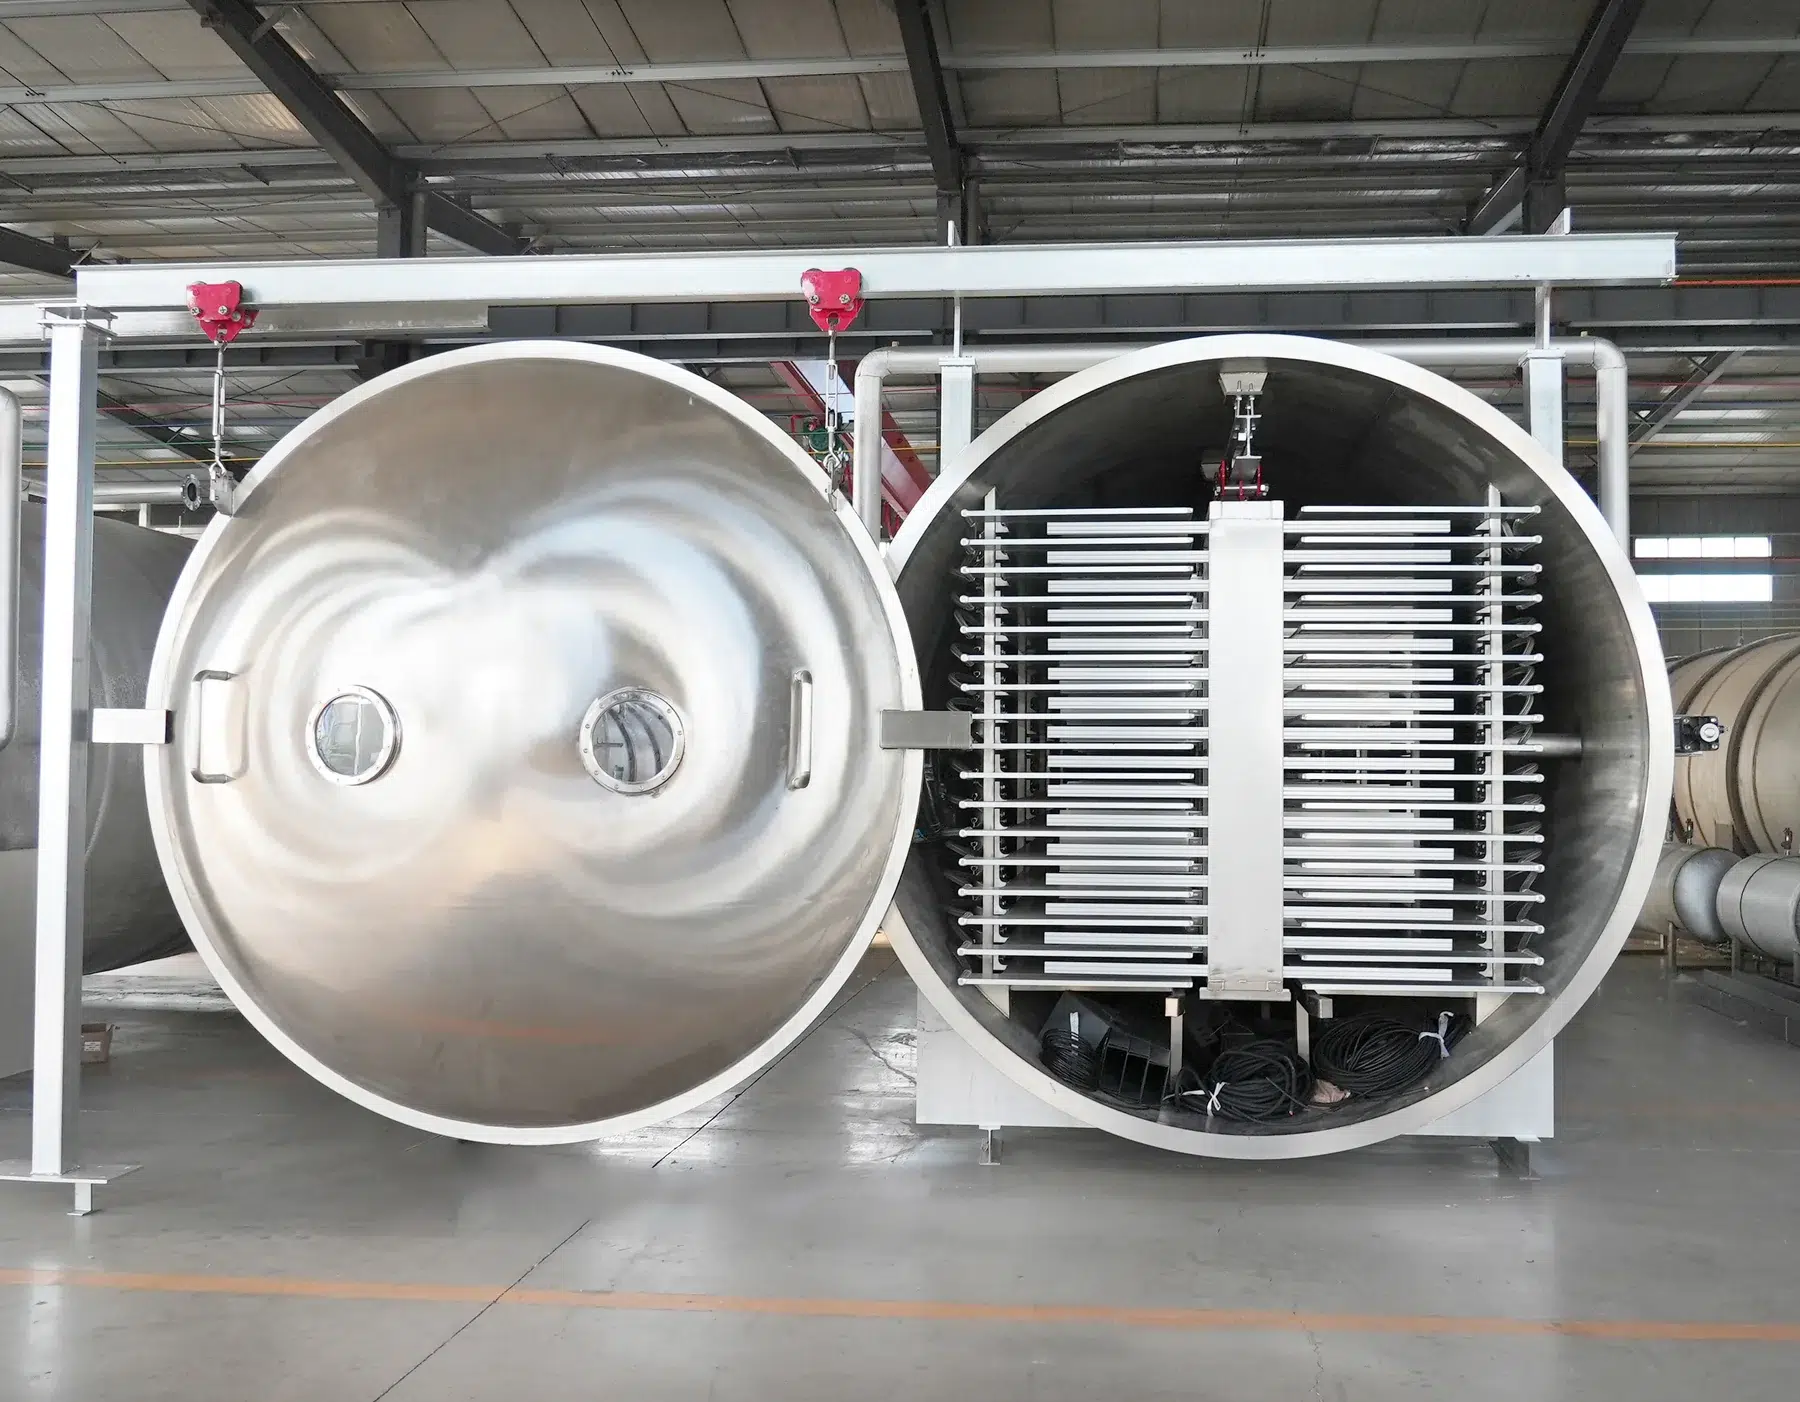
What we engineer
- Chamber volume and shelf area
- Condenser duty, which follows the peak water removal rate and not the batch weight
- Refrigeration and vacuum sizing
- Heating method — electric shelf, or steam and thermal fluid
- Defrost arrangement — single water, steam, or alternating automatic
- Automation depth and batch record scope
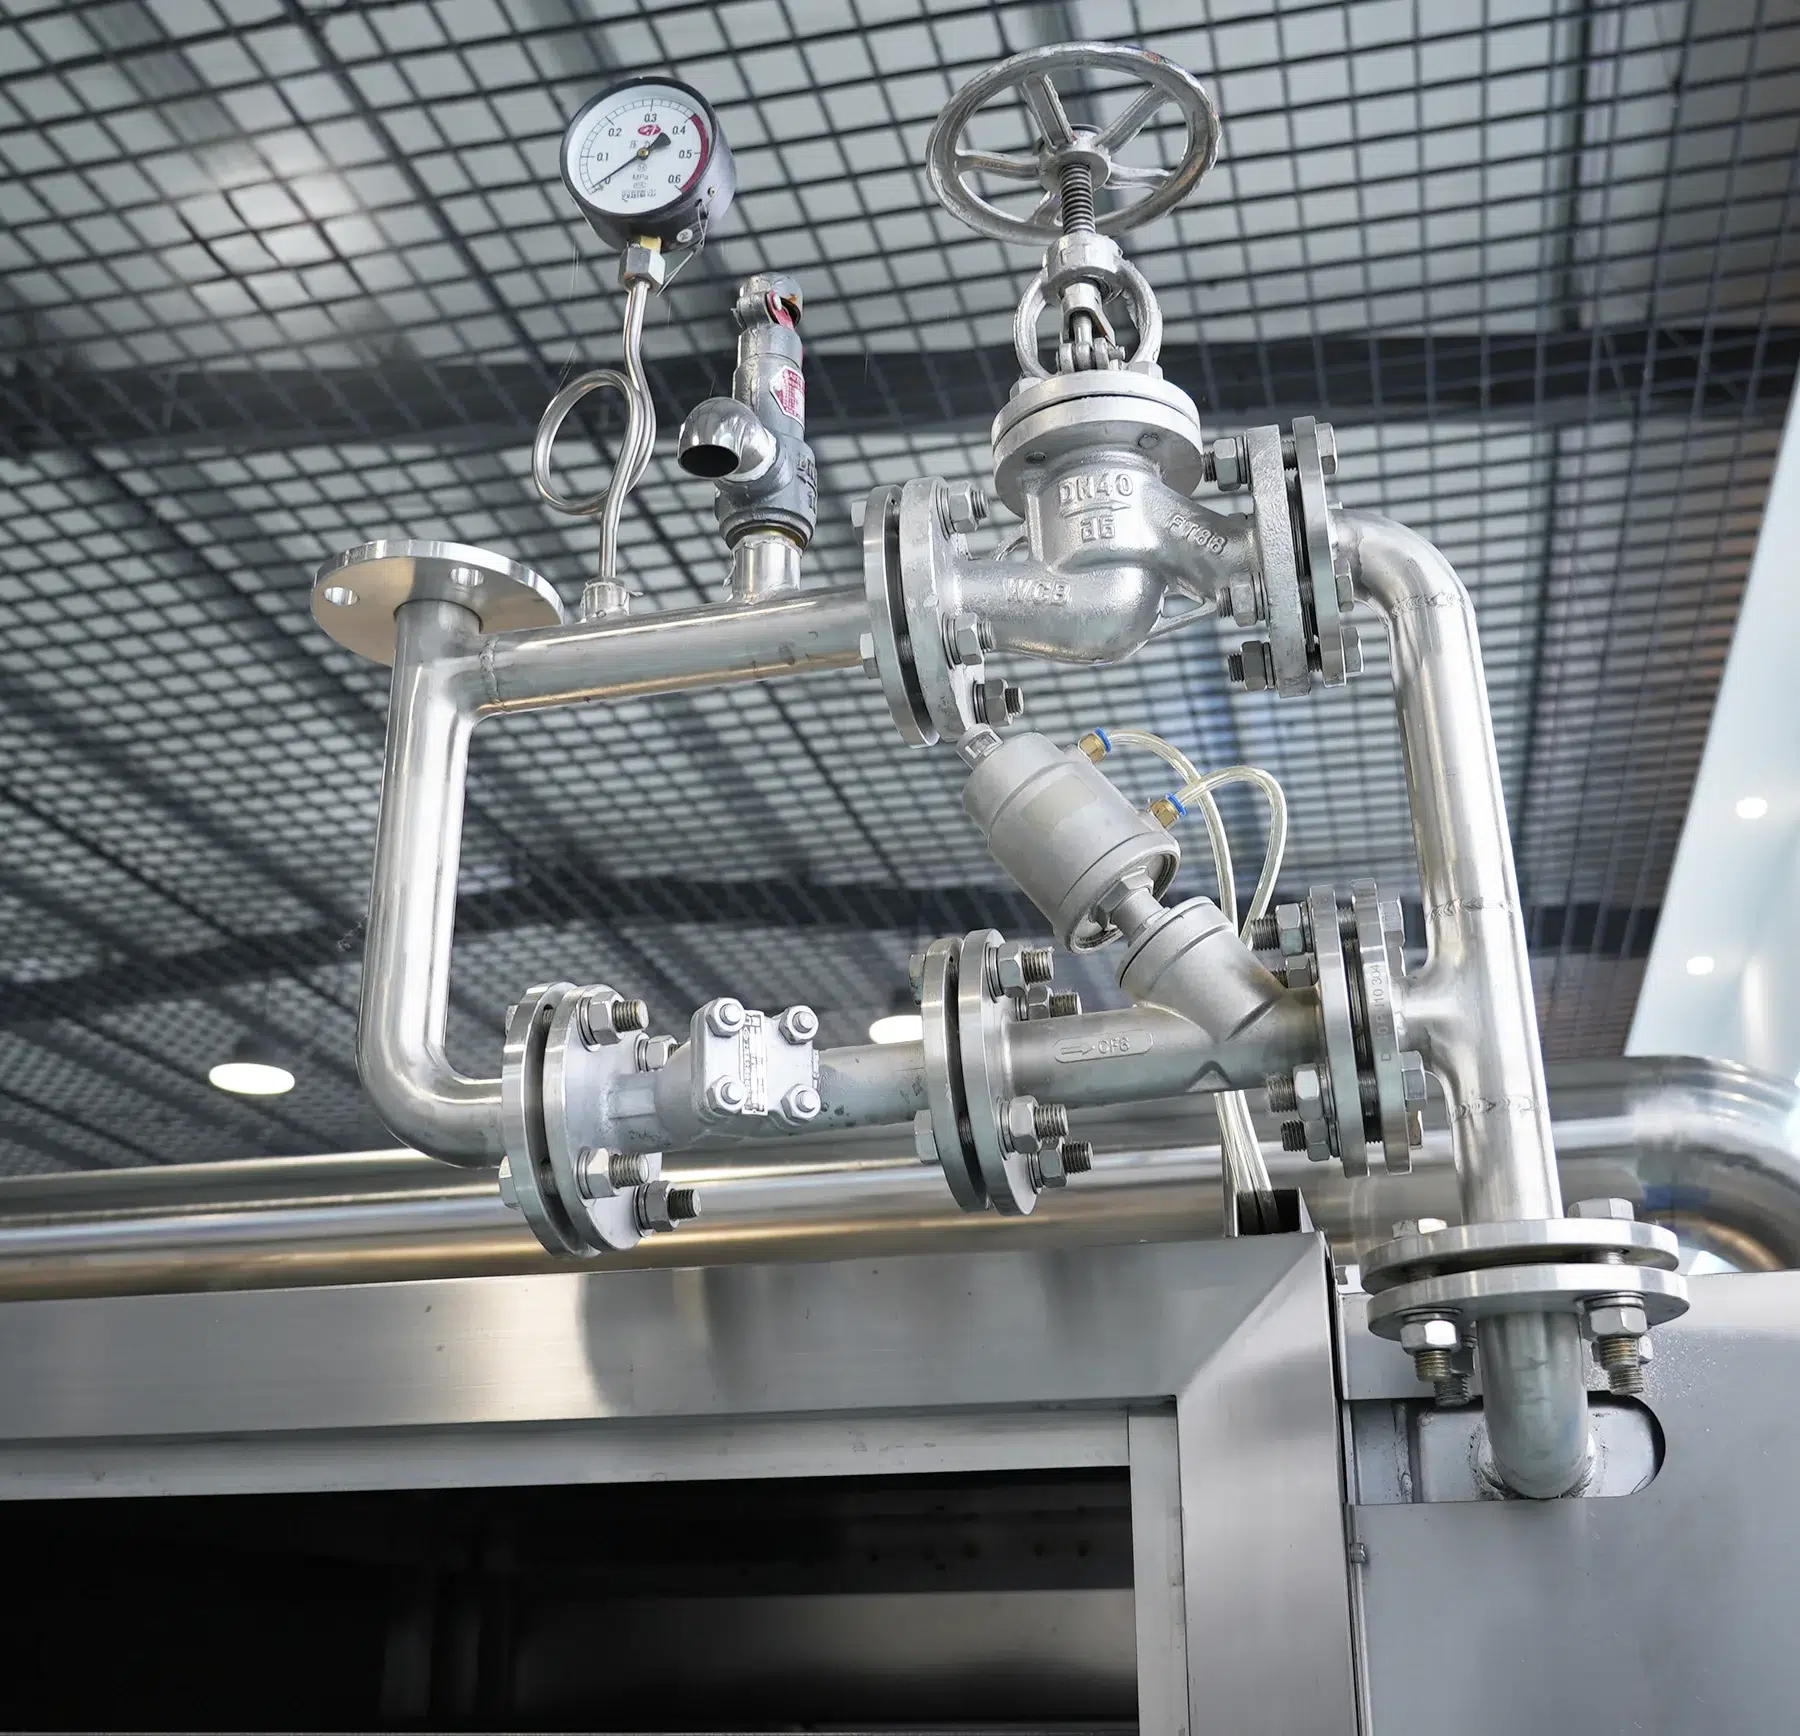
What the review hands back
- A configuration sheet carrying the shelf area, chamber volume and condenser duty the engineering review settled on
- A general arrangement drawing to sign off, which on the belt route is where the lead-time clock starts
- A utility requirement sheet issued in advance, so your contractor plans the supply rather than discovers it
- A sectional delivery and positioning plan, supplied alongside the configuration sheet
- The itemized quotation around all of it: equipment scope, documents supplied with the machine, packing and shipping method, and the acceptance arrangement
What an engineer needs from you before any of that can start is set out route by route in What to send for a quotation. Two of the calculators on the vacuum freeze dryer page compute shelf area and annual output from those same inputs, so the numbers you reach yourself and the numbers in the engineering review should agree.
Working out how much water actually has to leave. Put one product’s throughput and two moisture figures into the Water Removal Load Comparator and it returns an hourly duty on both routes, so you can see the load each machine family would carry.
Pricing Mechanism, Lead Time and Payment by Route
There is no price list for either route, because both machines are built to a product rather than to a catalog. Your figure follows drying area or shelf area and condenser duty, heat source, material grade, automation depth, and where the project scope stops. A published commercial freeze dryer price would have to assume a product, a load and a scope boundary, and any one of the three being wrong makes the number useless to you.
Hourly water load
Effect on cost
The real size driver on both routes. Throughput multiplied by the gap between inlet and outlet moisture sets how much water must leave per hour.
To bring it down: Remove free water upstream with a dewatering or centrifugal step.
Drying area or shelf area
Effect on cost
Area is the largest single cost driver, since structure, heating and handling all scale with it.
To bring it down: Fix loading density by trial before sizing, stack belt layers.
Heat source
Effect on cost
Capital and running cost pull in opposite directions. Electric is cheapest to install and dearest to run.
To bring it down: Choose against your local energy price and existing steam capacity.
Material grade
Effect on cost
SUS 316 contact surfaces cost more than SUS 304.
To bring it down: Specify 316 for the contact side only, rather than the whole machine.
Defrost arrangement
Effect on cost
On the freeze-drying route, alternating automatic defrost costs more to build.
To bring it down: Only worth it if you will actually run the extra batches.
Scope boundary
Effect on cost
Blast freezing, trolleys, loading rails and packing can double a project.
To bring it down: Ask for the quotation itemized so you can stage the purchase.
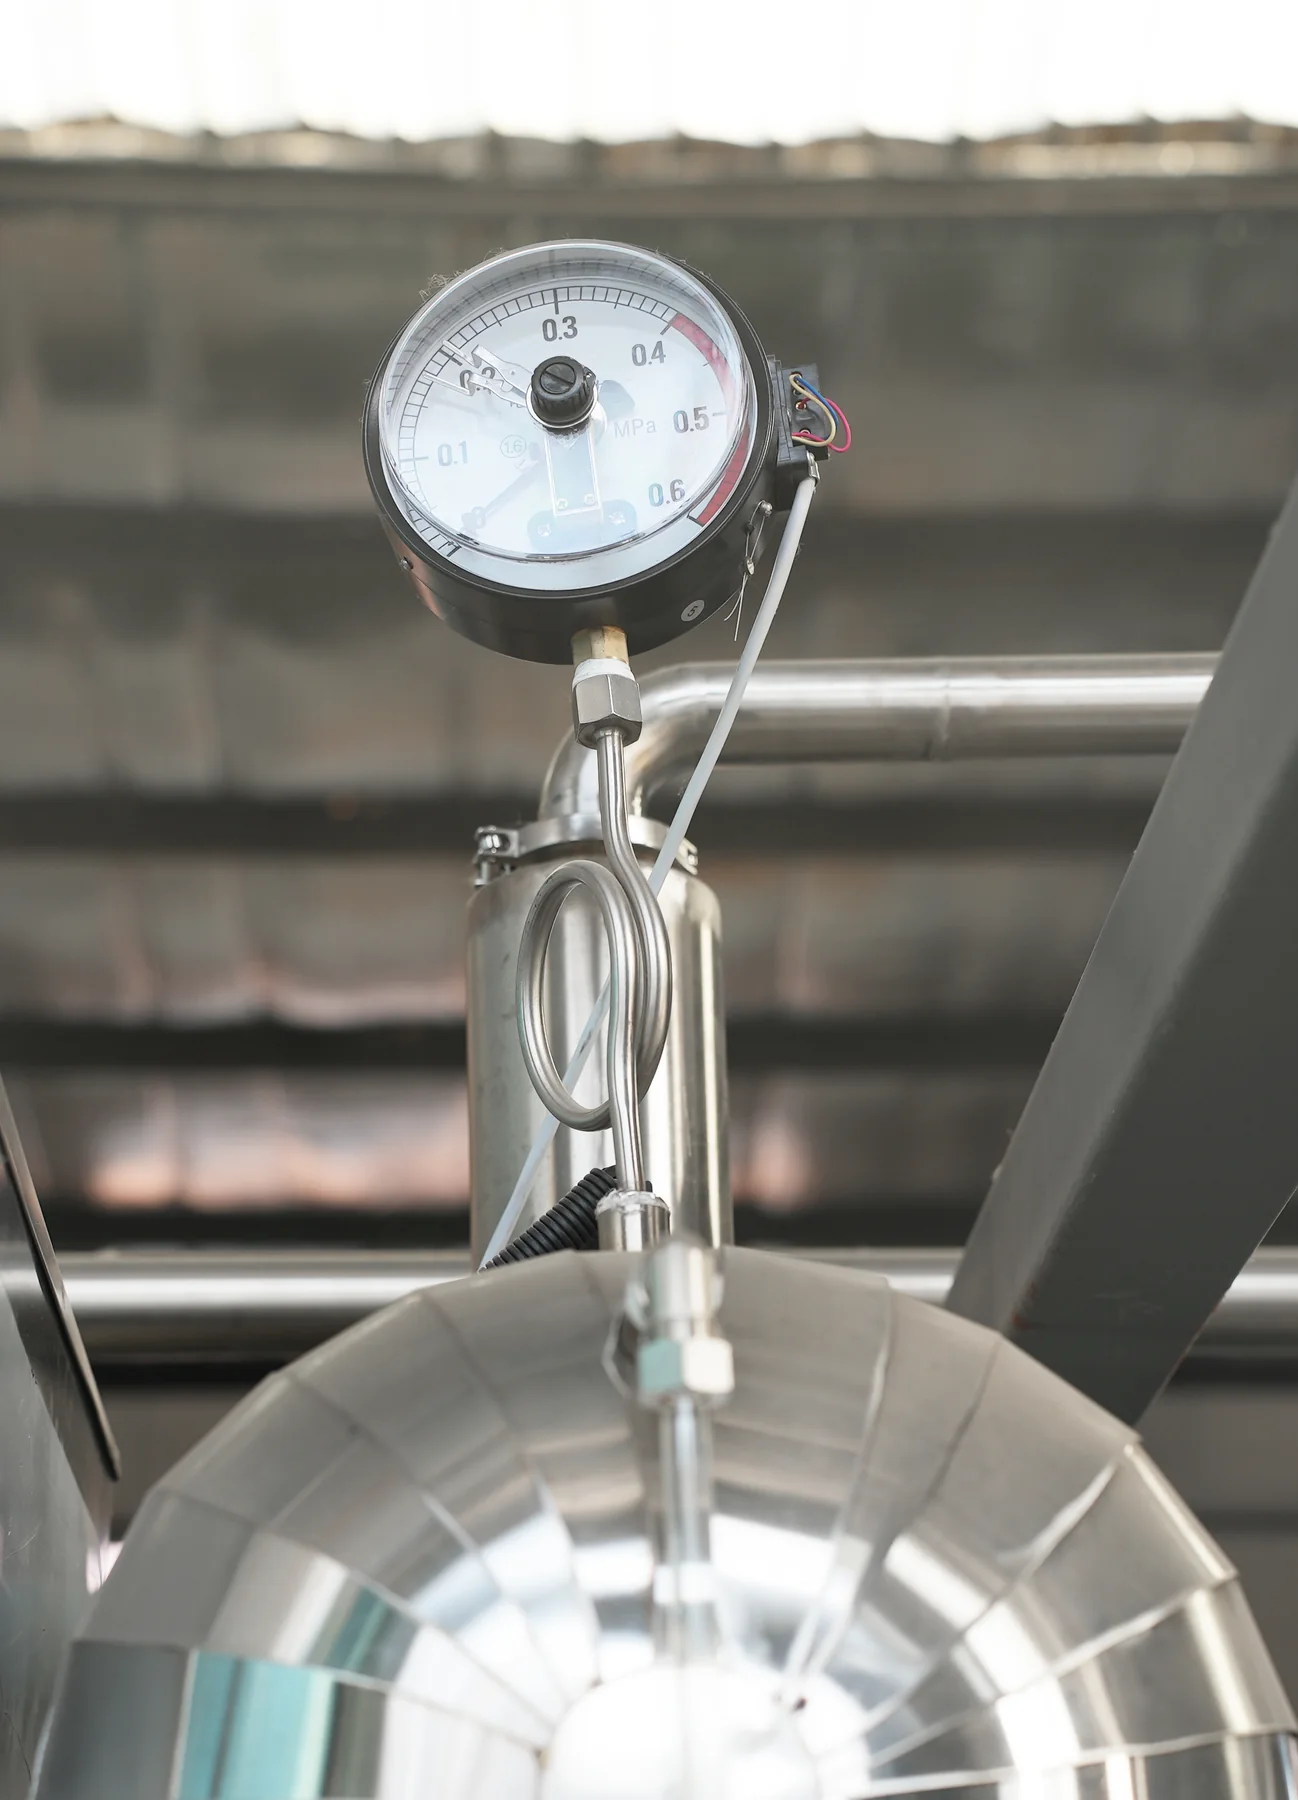
| Term | Mesh-belt hot-air dryer | Vacuum freeze dryer |
|---|---|---|
| Quotation turnaround | Within 24 hours, with proposal, layout suggestion and energy estimate | Issued after an engineering sizing review of your product data |
| Lead time | 30–40 working days for one standard machine; 30–60 working days customized or line-integrated, counted from drawing approval | 60–120 working days from the date the deposit clears |
| Payment | 30% deposit, balance before shipment, by bank transfer | Telegraphic transfer against a deposit at order confirmation, or a letter of credit |
| Warranty | Warranty duration, coverage and exclusions are confirmed in the quotation and contract | Warranty duration, coverage and exclusions are confirmed in the quotation and contract |
| Minimum order | One machine | One machine |
| Support response | Response times, remote support, on-site service and spare-parts arrangements are confirmed in the quotation and contract | Remote access through the control platform so our engineers read alarms and recipe logs with you |
Lead time on both routes excludes transit. On the belt route the clock starts when you sign off the general arrangement, not when the inquiry arrives.
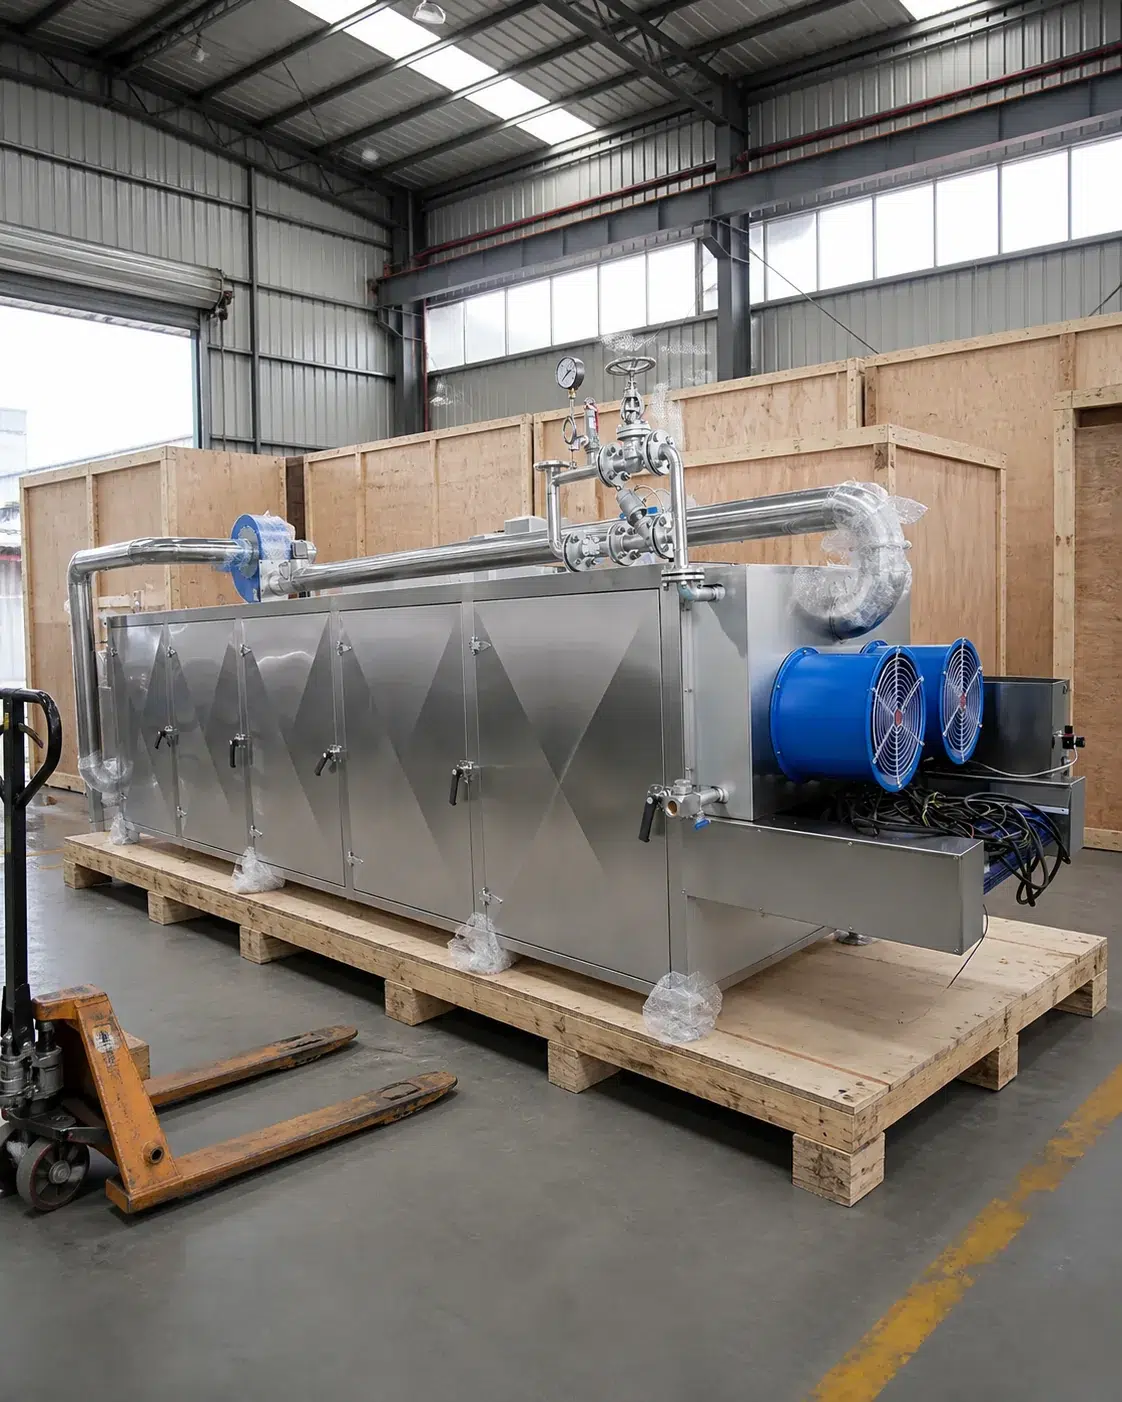
| What an engineer needs | Mesh-belt hot-air dryer | Vacuum freeze dryer |
|---|---|---|
| Product | The product | The product and the cut it is prepared to |
| Rate | Target throughput in kg/h | The output you need and the operating days behind it |
| Moisture | Inlet and outlet moisture targets | Incoming moisture, target residual moisture, and the water activity you have to prove |
| Utilities | Heat source available on site | Utilities available, including whether a steam supply exists |
| Space | Floor space you have for the machine | Ceiling height, floor loading and door run-out |
Vendor neutrality is published on our freeze-dryer route and it is how we build on both: we do not lock either machine to a single component brand. Where you already standardize on a refrigeration or control supplier for the rest of the plant, say so with your brief and we build to that requirement so your spares stay common.
Not sure what to prepare before asking for a price? Work through the Equipment Specification Checklist: it turns the items a food plant’s purchase specification should carry into a list you can send to us or to anyone you are comparing.
Factory Testing and Hygienic Construction
A dryer that has never run before it leaves the factory is one you will commission twice, and the risk is not shared evenly: a fault found in our workshop costs a shift, while the same fault found on your floor costs freight and a stalled line. That gap is structural, because once the machine ships every unresolved item turns from a test into a negotiation. So every machine Shengtu builds is run before packing against acceptance criteria written before it was built, and the results are recorded before shipping.
Factory test sequence
Mesh-belt hot-air dryer
- Fabrication check against the approved general arrangement, covering belt tracking, frame squareness and panel sealing
- No-load run of belt drive, fans, heating circuit and control system, watching for vibration, leakage and abnormal noise
- Heating and temperature uniformity test across zones, confirming each set point holds and neighboring zones do not fight each other
- Loaded trial run under simulated production conditions, verifying belt speed control and discharge behavior
- Full-machine interlock and safety test, then packing with the fasteners and spares needed for site assembly
Vacuum freeze dryer
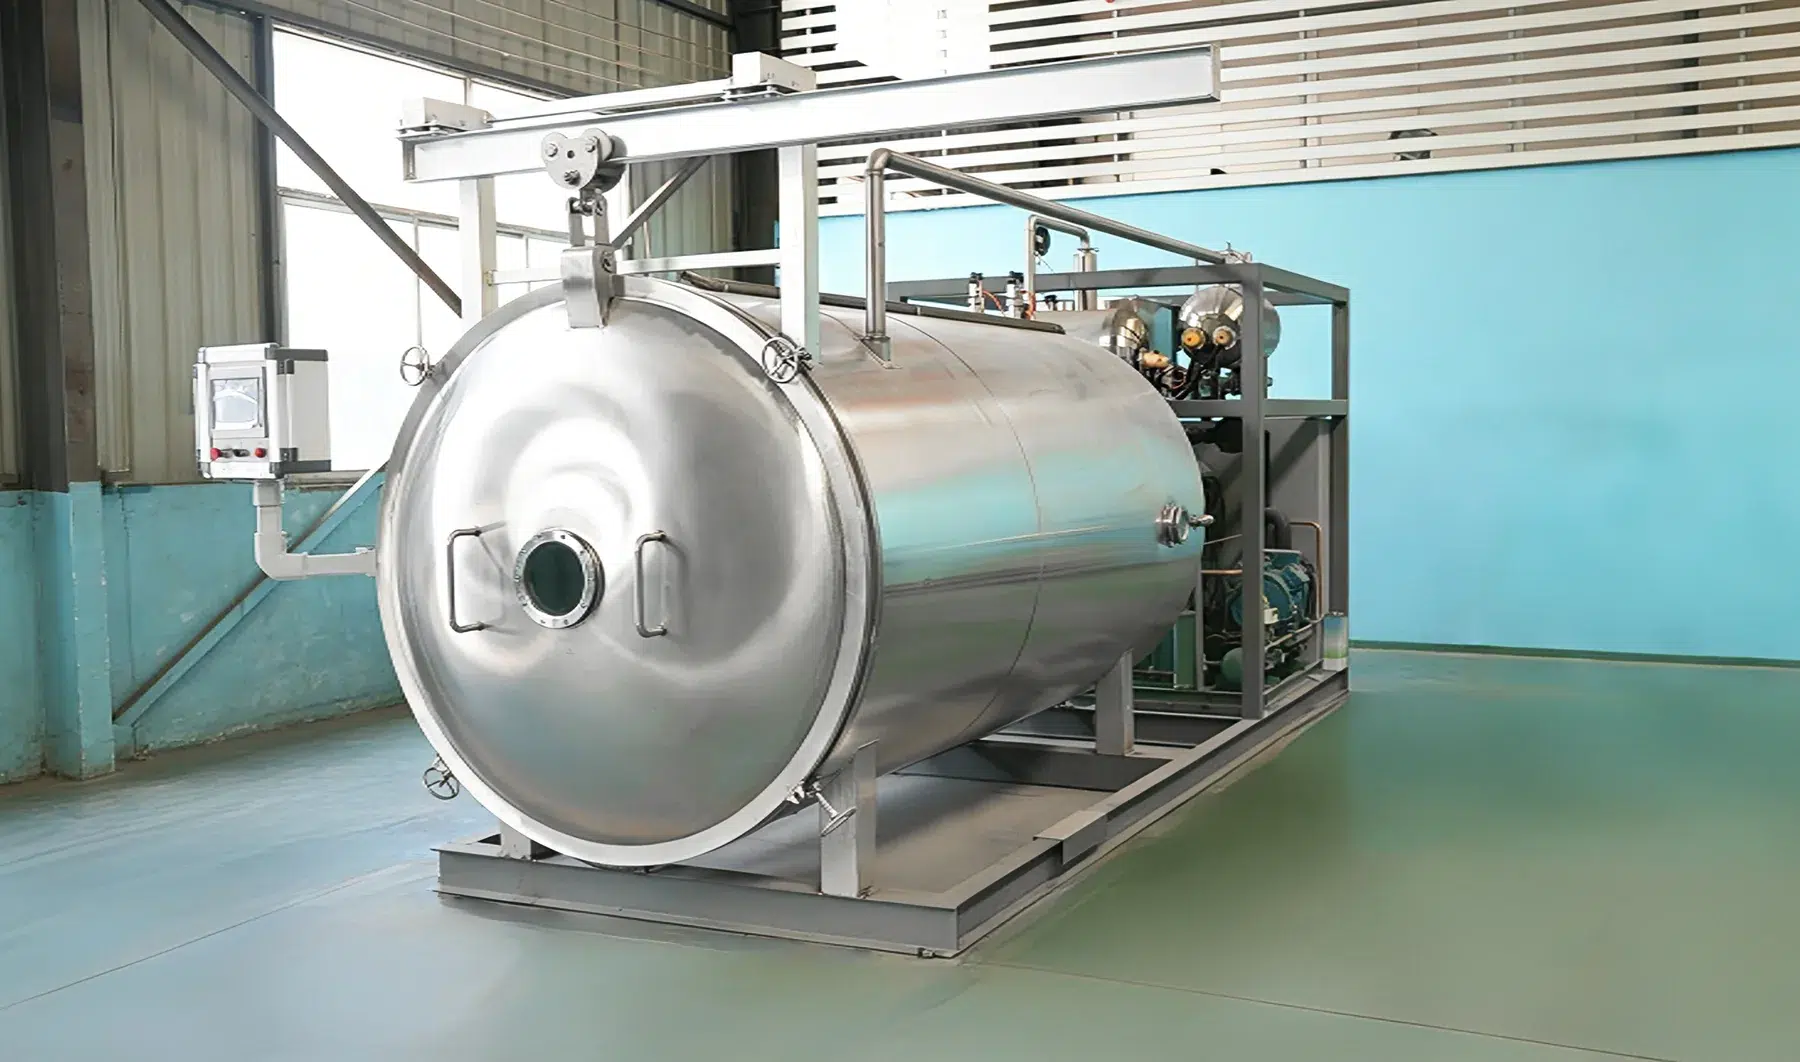
- Chamber and condenser welds inspected, then the assembly pressure and leak tested
- Vacuum pump set run and the empty chamber held under vacuum to confirm the seal
- Refrigeration charged, compressor set pulled down, condenser temperature confirmed against the recipe range
- Shelf heating stepped through its range with temperature logged shelf by shelf for uniformity across the stack
- Simulated run exercising the control sequence end to end before packing begins
Acceptance Criteria & Rework
If a checked item falls outside the approved drawing, we rework or remake it against the same written criteria used at the fabrication check.
Hygienic construction design criteria
US food regulation sets the standard this construction answers to, and the obligation it creates sits with the plant operating the equipment rather than with the machine builder. Equipment must be so designed and of such material and workmanship as to be adequately cleanable and adequately maintained to protect against allergen cross-contact and contamination, and food-contact surfaces must be corrosion-resistant when in contact with food.[3] We build to support that obligation; proving it in your facility remains yours.
How the machines answer it
- SUS 304 stainless steel is the standard build for frame, panels and contact surfaces
- SUS 316 is available where salt, acid or aggressive cleaning chemistry is part of the daily routine
- Belt material is stainless mesh or polyurethane, chosen by product contact and cleaning method
- Panels open for inspection so the belt run, the plenum and the fans can be reached without dismantling the tunnel
- The dryer can be tied into an existing clean-in-place system where the wider line already runs one
Why the zone sensors are a compliance item
The same regulation requires that instruments and controls used for measuring, regulating or recording temperature, pH, acidity, water activity or other conditions that control or prevent the growth of undesirable microorganisms in food be accurate and precise, adequately maintained, and adequate in number for their designated uses.[3]
- A drifting sensor is a silent failure: the display reads correctly while the load underneath it does not dry.
- That precision is verified zone by zone against set point during the factory heating test.
- The same instruments are re-checked during on-site commissioning before the first production run.
Company qualifications & Standards
- ISO 9001 quality management system
- ISO 27001 information security management system
- DCMM Level-2 data management capability maturity
These are company-level qualifications held by Shandong Shengtu Bufan Intelligent Technology. They describe how the business is run, and they are not product approvals for any individual machine.
Company records: Request the current holder, scope and validity details.
Equipment conformity: Confirm the documents for the model, configuration and destination country.
Order documents: Agree inspection records, manuals, drawings and shipment paperwork in the contract.
×
![Zoomed View]()
How We Work: From Product Brief to Commissioning
University food-process engineering guidance sets out what a plant’s equipment specification should contain, including a functional acceptance test before shipment, warranties and spare-parts lists among the submittals, and whether the supplier provides installation personnel and at what rates including travel and lodging.[8] The sequence below is written against those items.
Engineering Sequence
01
Send your product brief
Product, cut or piece size, inlet and outlet moisture, the output you need, heat source and floor space.
02
Engineering review
We convert the brief into an evaporation or water-removal duty and tell you what is missing before anything is priced.
03
Itemized written quotation
Equipment scope, configuration sheet, documents supplied with the machine, packing and shipping method, and the acceptance arrangement.
04
Drawing approval
You sign off the general arrangement, and on the belt route the lead-time clock starts here.
05
Manufacture and factory testing
The test sequence above, completed and recorded before shipping; we do not consider the job done at delivery.
06
Installation, commissioning and operator training
Our engineers travel to your site to direct installation, complete commissioning and train your operators.
Who does what on site
| Item | Shengtu | Your plant |
|---|---|---|
| Sectional delivery and positioning plan | Supplied with configuration sheet | Access route and floor loading confirmed |
| Lifting gear, tools and skilled trades | — | Forklift, crane, welding equipment, welder, fitter, electrician |
| Assembly supervision | Our engineer directs the sequence on site | Your crew executes under that direction |
| Utilities to the machine | Requirements issued in advance | Power, water and any steam supply terminated at the machine |
| Commissioning and operator training | Carried out by our engineer through to a completed batch | Operators released to attend |
| Travel and accommodation | Quoted as a separate line | Confirmed with the order |

On the freeze-drying route the spare parts list is agreed at order, not after a stoppage, and wear items are named in the quotation with their replacement interval. On the belt route, spare-parts availability and dispatch arrangements are confirmed per order.
When Neither Route Is the Right Answer
Most equipment pages answer this question by widening the definition of what the machine does. Here is the honest version instead: both machines have a shape of product they cannot serve, and the mistake that costs a plant most is being sent to the wrong one rather than being turned away. The Drying Route Crossover decides between our two routes; this table is for the products that sit outside both, and each row names where the work should go instead.
Situation
Slurries, pastes and purées
Why it works against you
They flow through a perforated belt or blind the mesh, and a tray-loaded chamber turns a liquid into a handling problem.
What to do instead
Drum, spray or vacuum-belt drying. Spray drying in particular is sized by evaporation capacity rather than by chamber size.
Commodity dried goods sold on price
Why it works against you
Sublimation is the most energy-hungry step in the freeze-drying process,[1] and no configuration we build changes that.
What to do instead
The belt route for the commodity line, keeping freeze drying for the high-quality grade that carries the cost.
Very high sugar or high fat product on the freeze-drying route
Why it works against you
A low collapse temperature forces a slow shelf ramp, so the cycle stretches and daily output drops.
What to do instead
Reformulate, cut thinner, or size the machine for the longer cycle rather than being surprised by it.
Buying capacity to fix a line bottleneck
Why it works against you
A bigger dryer does nothing for annual output if freezing, loading, cutting or packing sets the pace.
What to do instead
Time the whole sequence first. Shortening changeover and defrost often buys more annual output than a larger machine.
Very short residence time or a powder end-product
Why it works against you
Neither of these two routes is built for seconds-scale drying or for producing a free-flowing industrial powder directly.
What to do instead
Microwave and radio-frequency drying, infrared, or hybrid systems — all outside this category.
Pharmaceutical lyophilization
Why it works against you
Sterile-boundary work, isolator integration and validated batch records are a different regulatory build entirely: that work sits under 21 CFR Part 211, Current Good Manufacturing Practice for Finished Pharmaceuticals, not under the food equipment rules this page works to.
What to do instead
A pharmaceutical freeze-drying supplier. Our machines are food-plant equipment and we say so rather than stretch the claim.
Drying Equipment Engineering Tools
Drying Route Crossover Check
Six axes decide whether a product belongs on the vacuum freeze drying route or the continuous mesh-belt hot-air route. Answer them for one product and this check reports which route to brief, and how clear the call is.
Access ToolEquipment Specification Checklist
Food-process engineering guidance lists what a plant’s purchase specification for processing equipment should carry. Tick what your specification already covers to build your gap list, plus generate a plain-text block for supplier briefing.
Access ToolWater Removal Load Comparator
Throughput on its own does not size a dryer. What sizes it is how much water has to leave. This tool converts one product’s numbers into the mass-balance load each drying route would carry.
Access ToolFAQ for This Freeze Dryer and Dryer Category
They are the same machine under two names, and either name sits on the same side of The Drying Route Crossover. Lyophilization is the technical term for the process, and freeze dryer is what the equipment is called in food plants. Pharmaceutical suppliers tend to use the first word and food equipment builders the second.
On the freeze-drying route it is the fresh product a chamber can load and dry in one batch, not the weight of finished product that comes out; on the belt route it is an hourly evaporation duty, which is throughput multiplied by the gap between your two moisture figures. Raw high-moisture produce carries 80 to 95 percent water, so on those products most of what leaves the chamber is water.[4] Raw beef and poultry cuts run lower, at 56 to 73 percent on USDA’s published figures, so a jerky or pet-treat brief and a berry brief size differently on the same chamber.
No. Moisture percentage is how much water is present; water activity is how available that water is to microorganisms, and it is the condition US regulation names alongside temperature, pH and acidity as something instruments must measure accurately.[3] Two products at the same moisture percentage can sit at different water activities. Your target and the evidence that proves it belong to your food-safety owner, and we size the secondary drying stage against the figure you set.
No. Drying is a dehydration and stabilization step, not a lethality step. For products such as jerky the lethality treatment sits before the dryer in your process, and both the process definition and the acceptance criteria belong to your destination-market food-safety owner.
Belt-route cycles run 6–15 hours on the reference configuration, and where a product lands inside that band is set by piece size, starting water content and the moisture endpoint. On the freeze-drying route the cycle has to be established by trial on your own product, and it is the single number that decides annual output.
Three things account for most of it: an uneven bed depth at the infeed, air short-circuiting through a thin patch instead of passing through the whole load, and a zone set point fighting its neighbor. None of the three is a machine defect. All three are set-up problems, which is why the loaded trial run and the on-site commissioning both exist.
Supply voltage and frequency are set against your site at drawing stage, and the general arrangement records what the machine is built to. Electrical approval in the destination market sits with your authority having jurisdiction and with the contractor performing the installation, and we issue the utility requirement sheet in advance so that work can be planned rather than discovered at commissioning.
Four questions separate a supplier quoting a machine from one quoting a picture. Ask which route they would put your product on and why; ask for the hourly water-removal or evaporation duty the machine is sized to rather than a kilogram-per-hour headline; ask what the lead time is counted from; and ask who performs the acceptance check and against what written criteria. A supplier who answers all four in writing has read your product data.
The honest version of that question is not about the country, it is about what happens after the machine lands. Our answer is written into the terms on this page, and it differs by route.
Belt route — response timing, remote assistance, on-site support and spare-parts availability are confirmed in the quotation and contract.
Freeze-drying route — remote access through the control platform, so our engineers read alarms and recipe logs with you.
Both routes — installation directed by our own engineers, with travel and accommodation quoted as a separate line so there is no surprise on the final invoice.
There is no price list for either route, because both machines are built to a product rather than to a catalog. Drying area or shelf area, condenser duty, heat source, material grade, automation depth and where the project scope stops all move the number more than anything else, and each of those drivers is set out with how to bring it down in Pricing Mechanism, Lead Time and Payment by Route. A figure quoted before anyone has read your product data is a figure for somebody else’s machine.
Plan for a three-phase supply, cooling water, and a steam supply if you choose steam heating. You also need ceiling height for the chamber plus lifting clearance above it, floor loading confirmed by your structural engineer, and clear run-out space in front of the door for trolleys. We issue the requirement sheet before delivery so your contractor can work to it.
Only where the product’s price supports it. Freeze drying holds shape, color, aroma and structure and reaches a lower residual moisture, and it costs more per kilogram of water removed to do it. Published work is blunt that a large class of products is not economically justified for freeze drying.[2]
Yes. Working height, discharge direction, the control interface and the mechanical boundary with the stations either side are fixed at drawing stage, which is the point at which changes cost nothing.
The quotation states the documents supplied with the machine, the packing and shipping method and the acceptance arrangement, so the list is confirmed in writing before you order rather than described in general terms here.
Yes. On the freeze-drying route the spare parts list is agreed at order, and wear items are named in the quotation with their replacement interval. Where a part is a standard industrial component rather than something proprietary to us, we say so, because that means you can source it locally as well as from us.
Sometimes, and the trade-off is the same on both routes. A used commercial freeze dryer or a second-hand belt tunnel was sized for somebody else’s water load, and re-sizing shelf area or belt area on an existing machine usually costs more than the discount saves. Chamber volume and belt length on their own tell you nothing about how long your own product will take.