Get in touch with Shengtu Bufan Company
Fruit and Vegetable Processing Lines
Four production lines, 200–3,000 kg/h depending on crop
We build fruit and vegetable processing lines for four kinds of work: washing and peeling root crops, fresh-cut leafy produce, hot-air dehydration, and freeze-drying. Three things decide which line fits you — the crops you run, the throughput you need, and the form your finished product leaves in. Send those three and we route you to a line instead of to a catalogue.
Core Highlights
- 60–90 days after configuration and layout approval
- 30% deposit and 70% before shipment by T/T
- Roughly 80% of core equipment built in our own plants
See Throughput by Crop
Send the crop and the target kg/h and we come back with a line route within one business day.
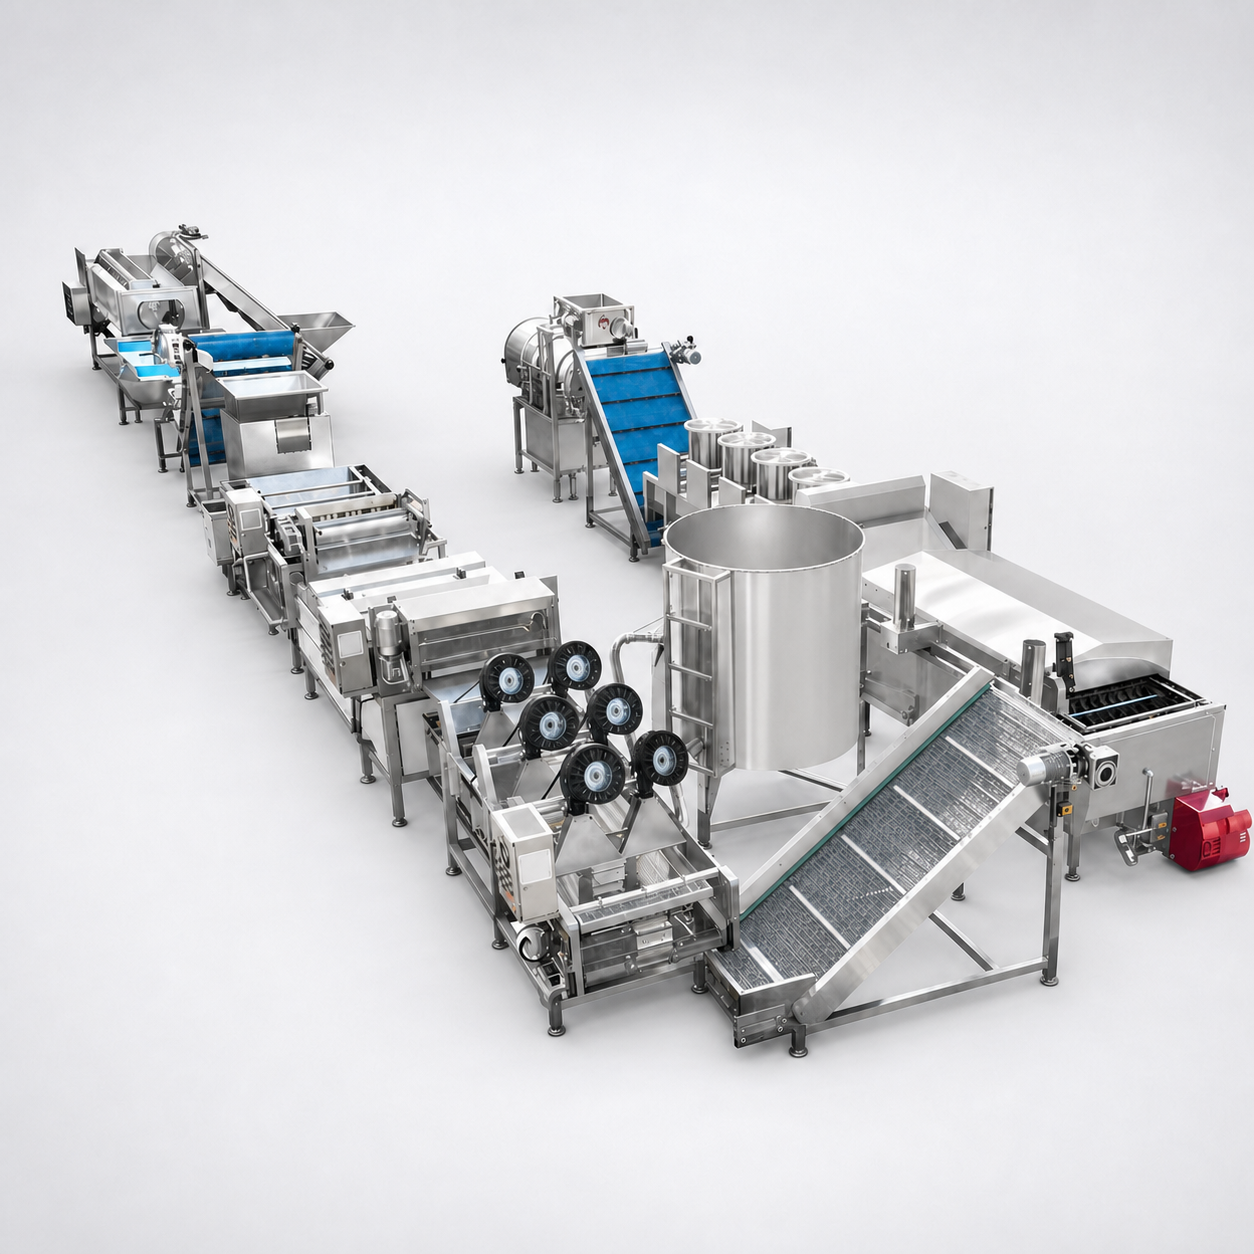
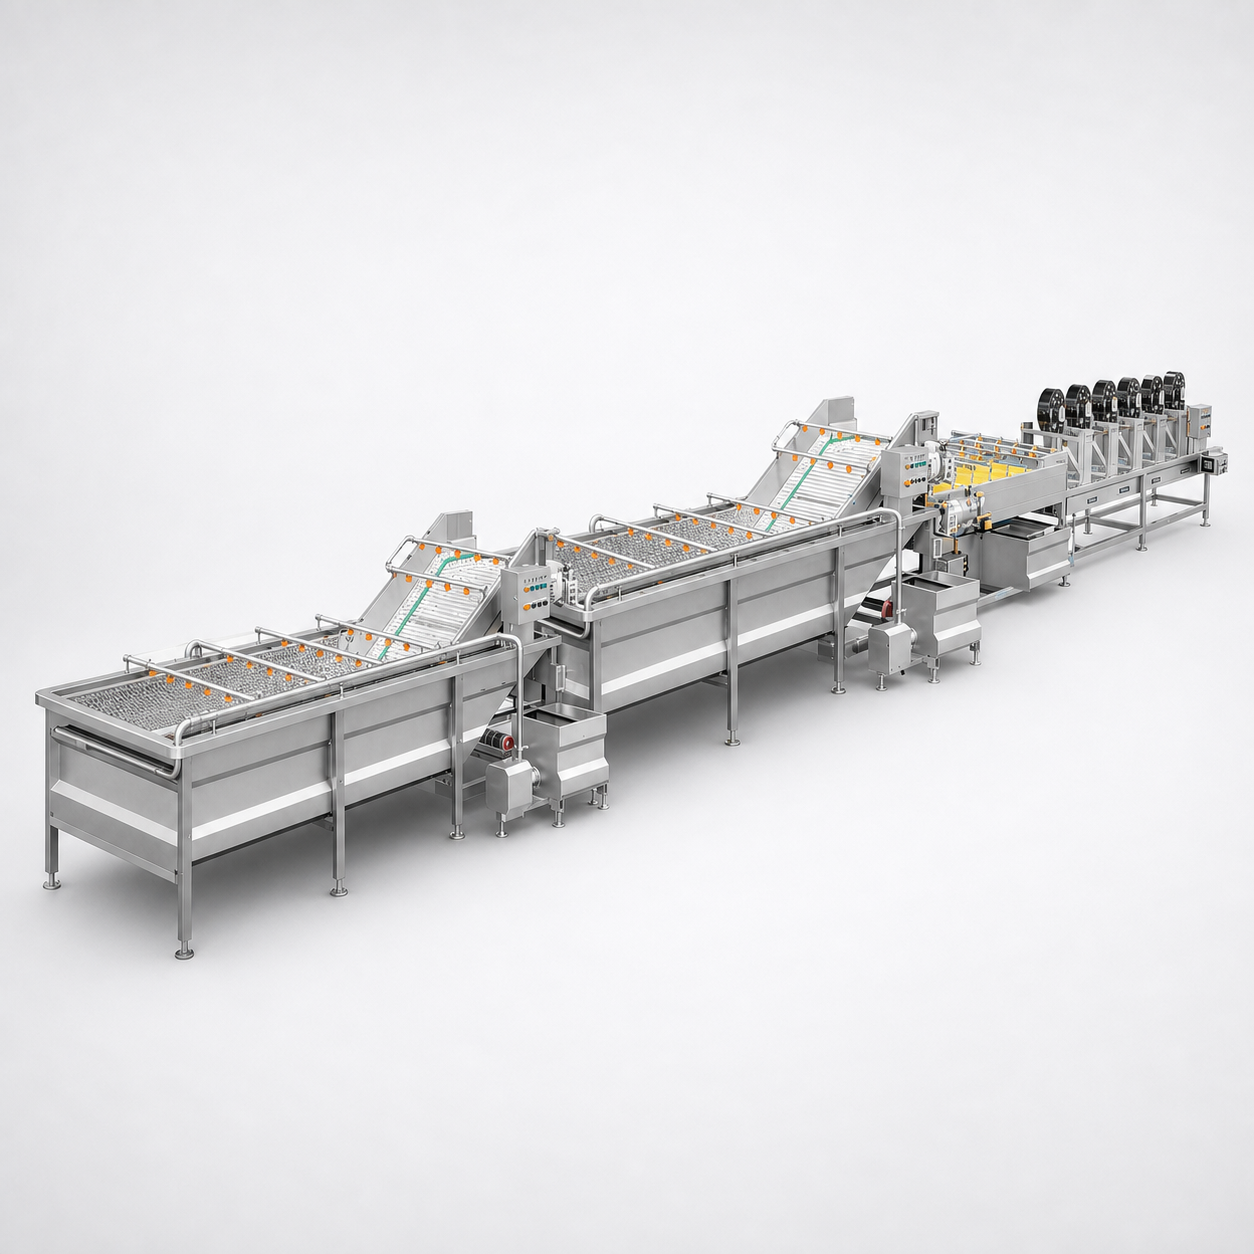
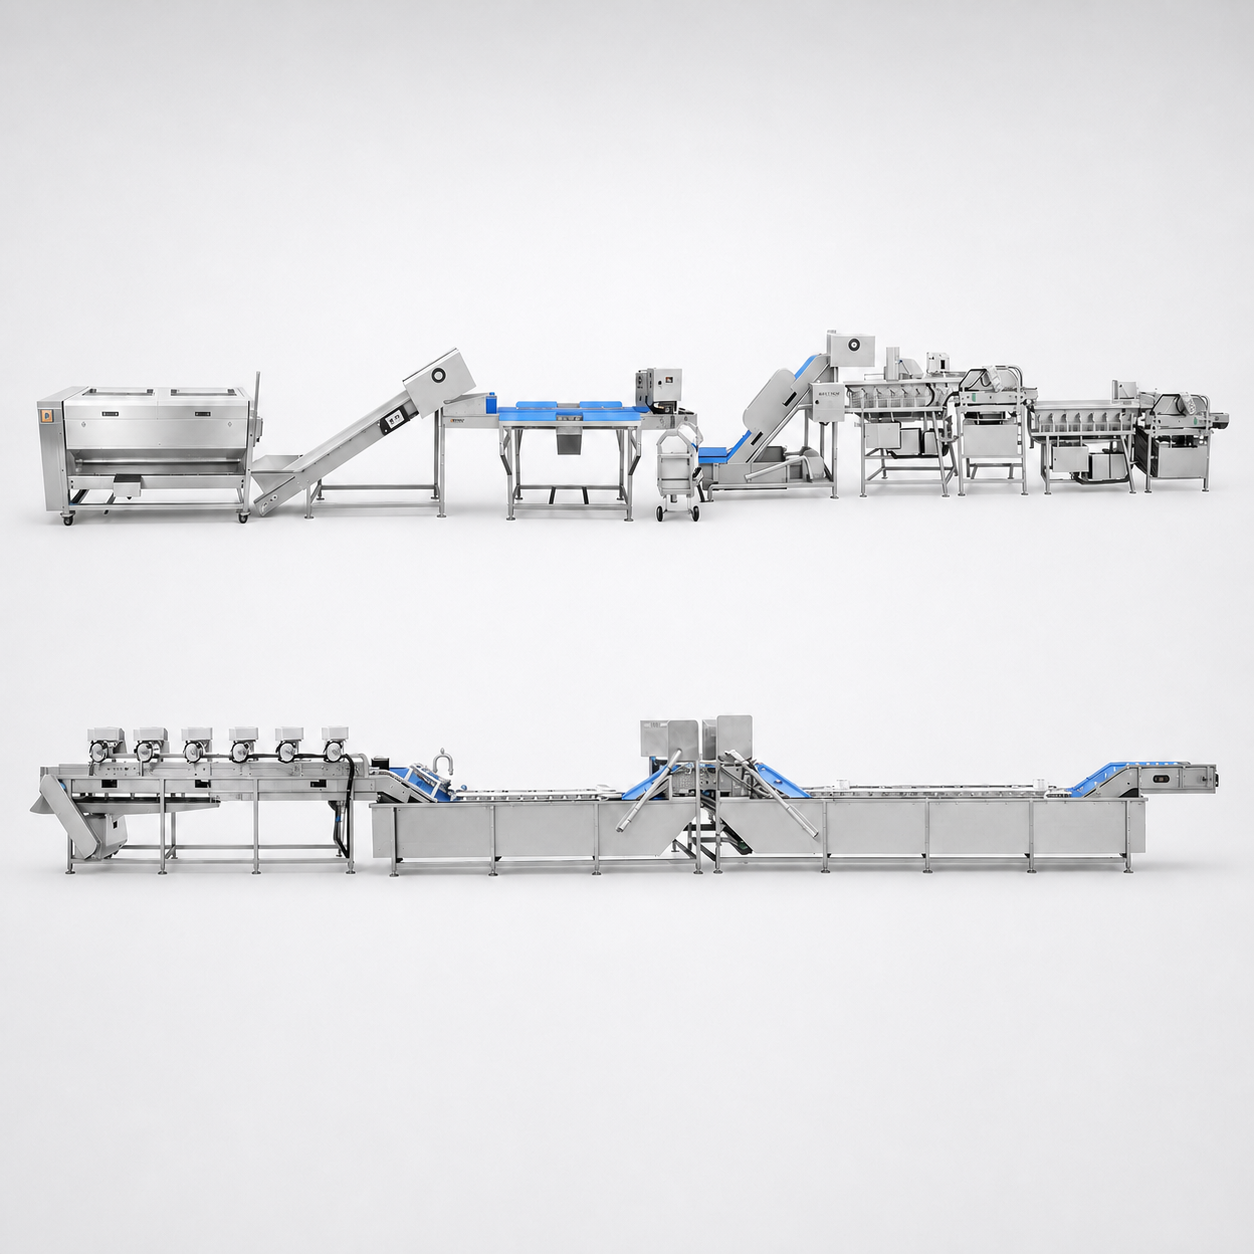
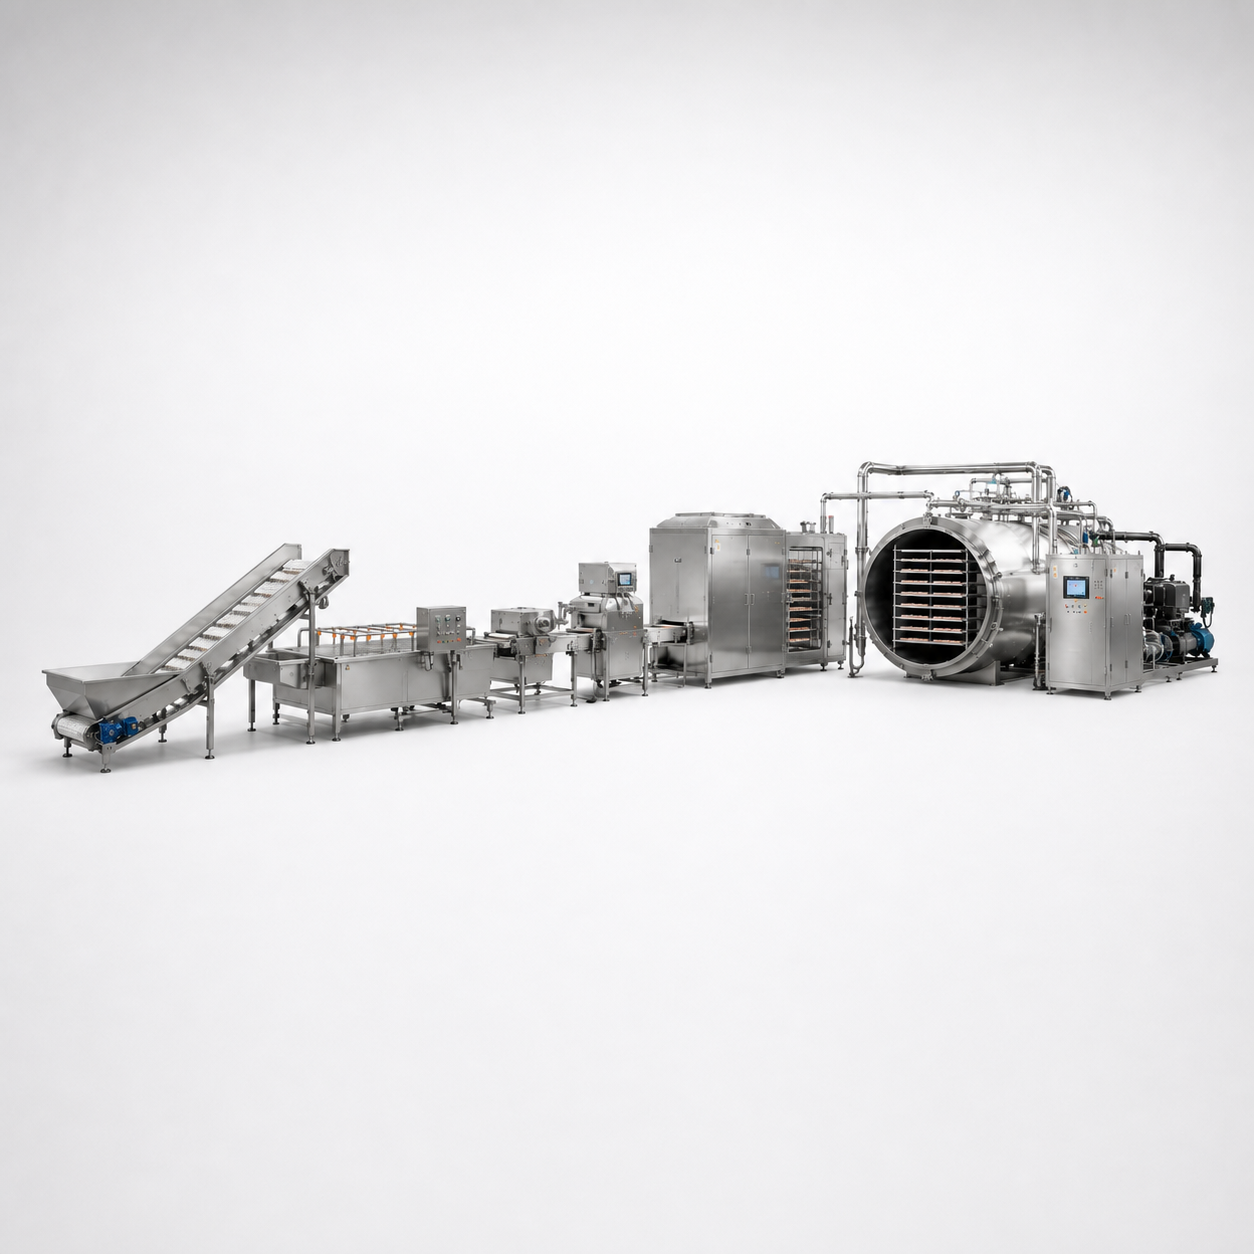
Line Configurations Gallery
Technical Specifications
Lines we build
Root vegetable washing/peeling, leafy fresh-cut, dehydration, freeze-drying
Throughput envelope
200–3,000 kg/h, set by crop and product form
Product-contact
Food-grade stainless steel, 304 standard, 316L on request
Response time
We answer a crop-and-throughput enquiry within 1 business day
Build window
60–90 days after configuration and layout approval
Where it is made
Four owned and self-built manufacturing bases; 20,000+ m² of office and display space across four cities
Four Fruit and Vegetable Processing Lines, Routed by Crop, Throughput and Product Form
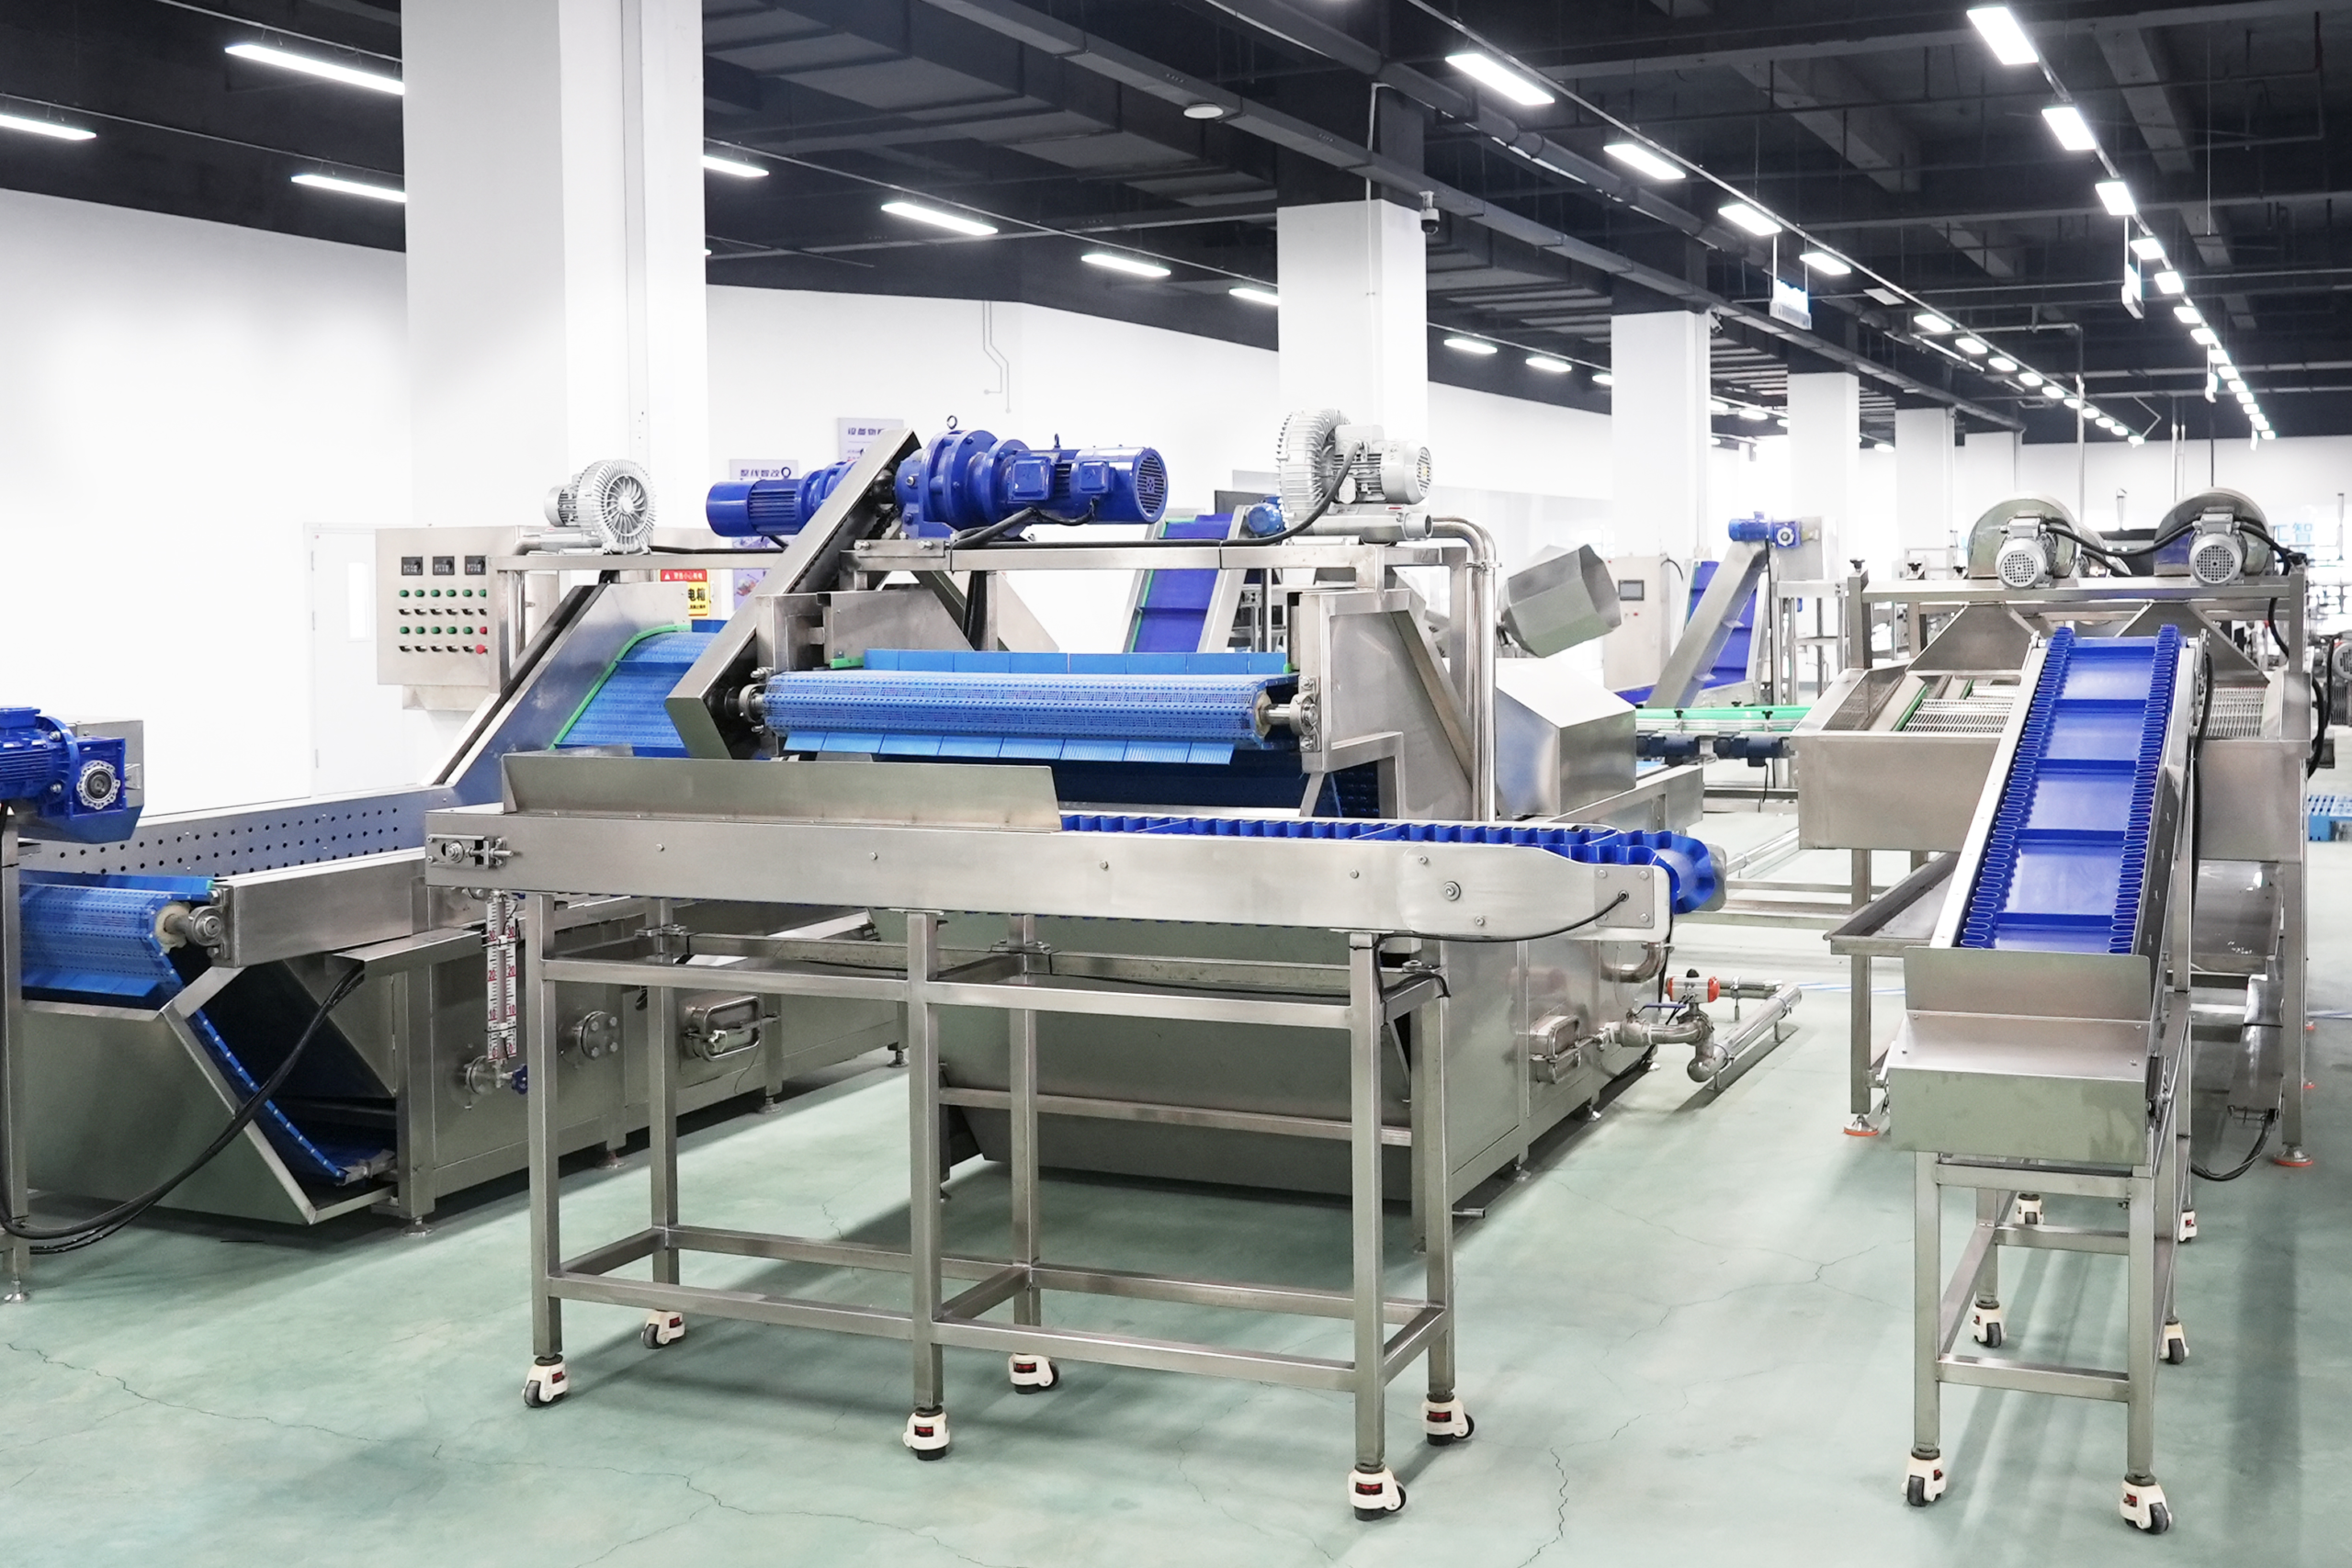
A fruit and vegetable processing line is not one machine but a station sequence, and that sequence gets decided before any equipment is quoted. Four standard sequences carry the work, and we customize the stations inside them. Our grid below is how we route an enquiry.
| What you run | What you want out | Line that fits | Stations |
|---|---|---|---|
| Potato, sweet potato, cassava, taro, carrot, radish, beetroot, onion, ginger, lotus root | Washed whole produce, or peeled sticks, slices and dice | Root vegetable washing and peeling line | 9 |
| Lettuce, cabbage, spinach and other leafy greens | Washed, dewatered, packed fresh-cut salad | Leafy fresh-cut line | 8 |
| Fruit and vegetables that hold shape when heated | Hot-air dried slices, dice, flakes and powders | Fruit and vegetable dehydration drying line | 7 |
| Fruit and vegetables sold on colour, aroma and shape | Freeze-dried pieces for snacks and ingredients | Fruit and vegetable freeze-drying line | 6 |
Root Vegetable Washing and Peeling Line
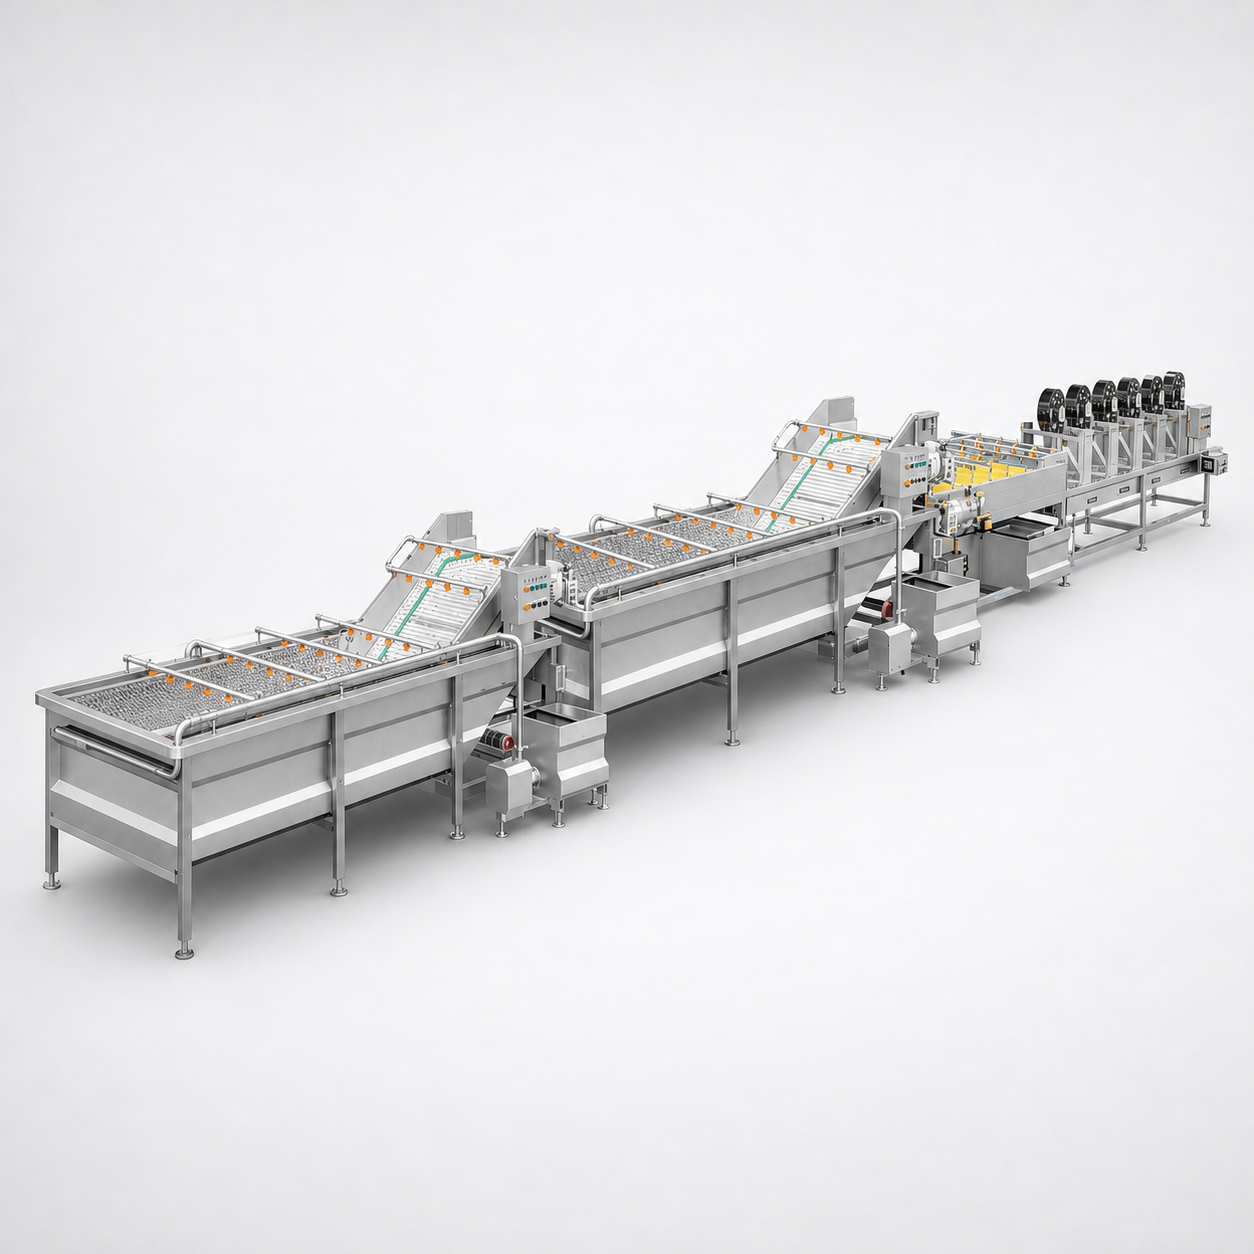
Intake and pre-sorting, pre-wash, de-stoning, peeling, sorting and inspection, cutting, post-wash with colour protection, dewatering, packing.
Leafy Fresh-Cut Line
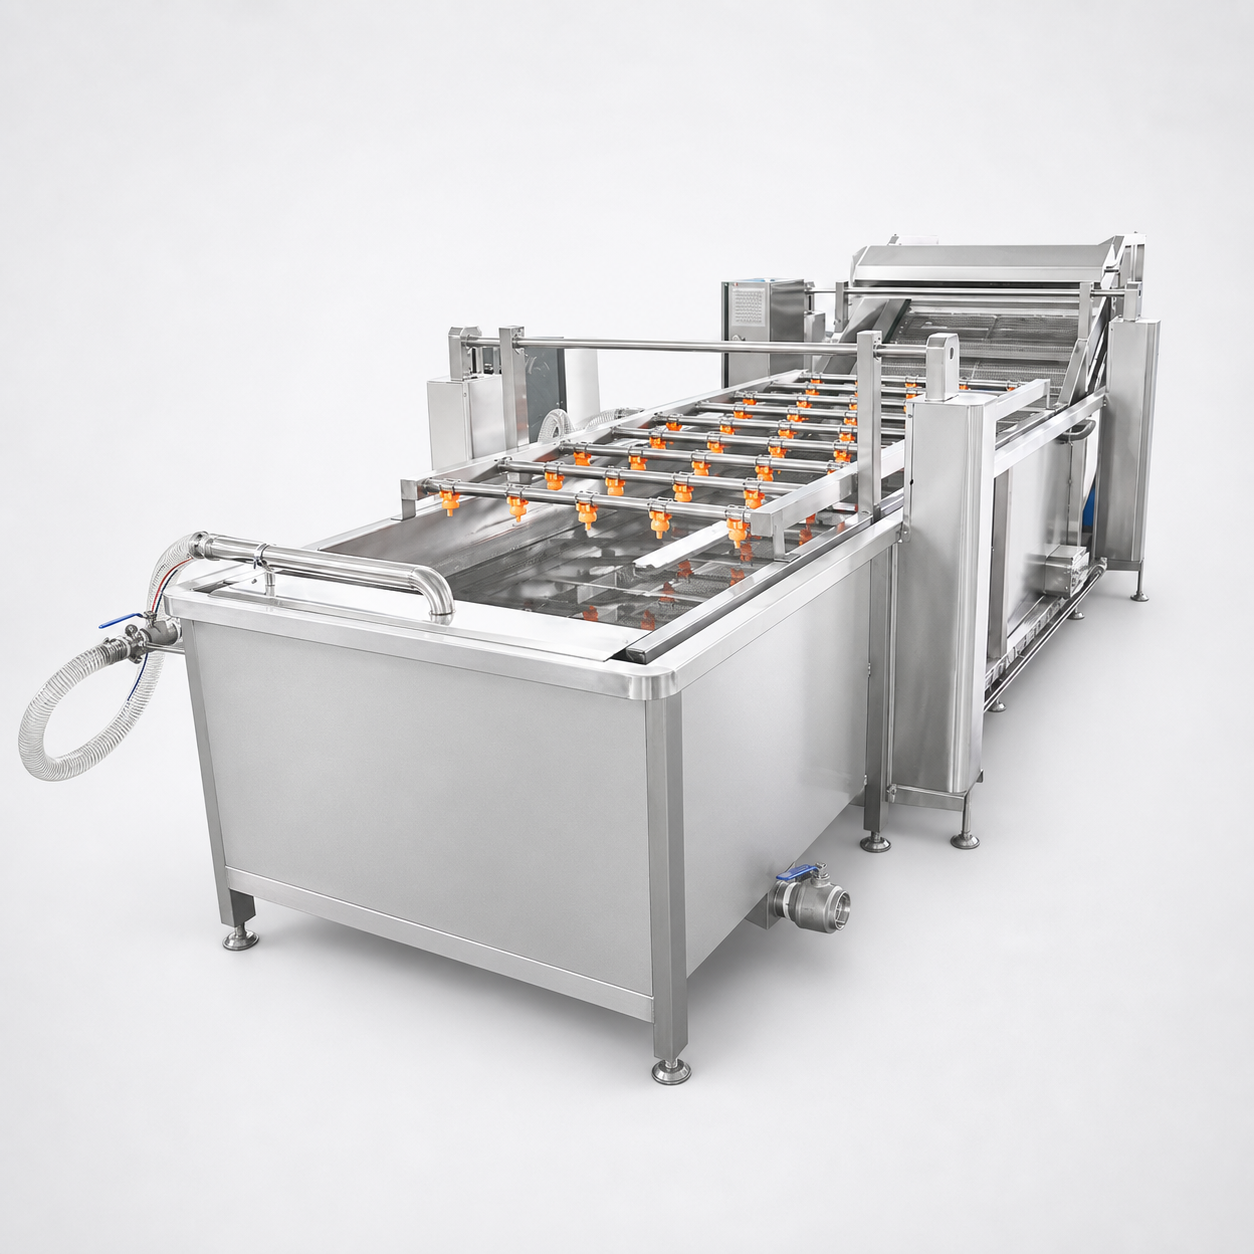
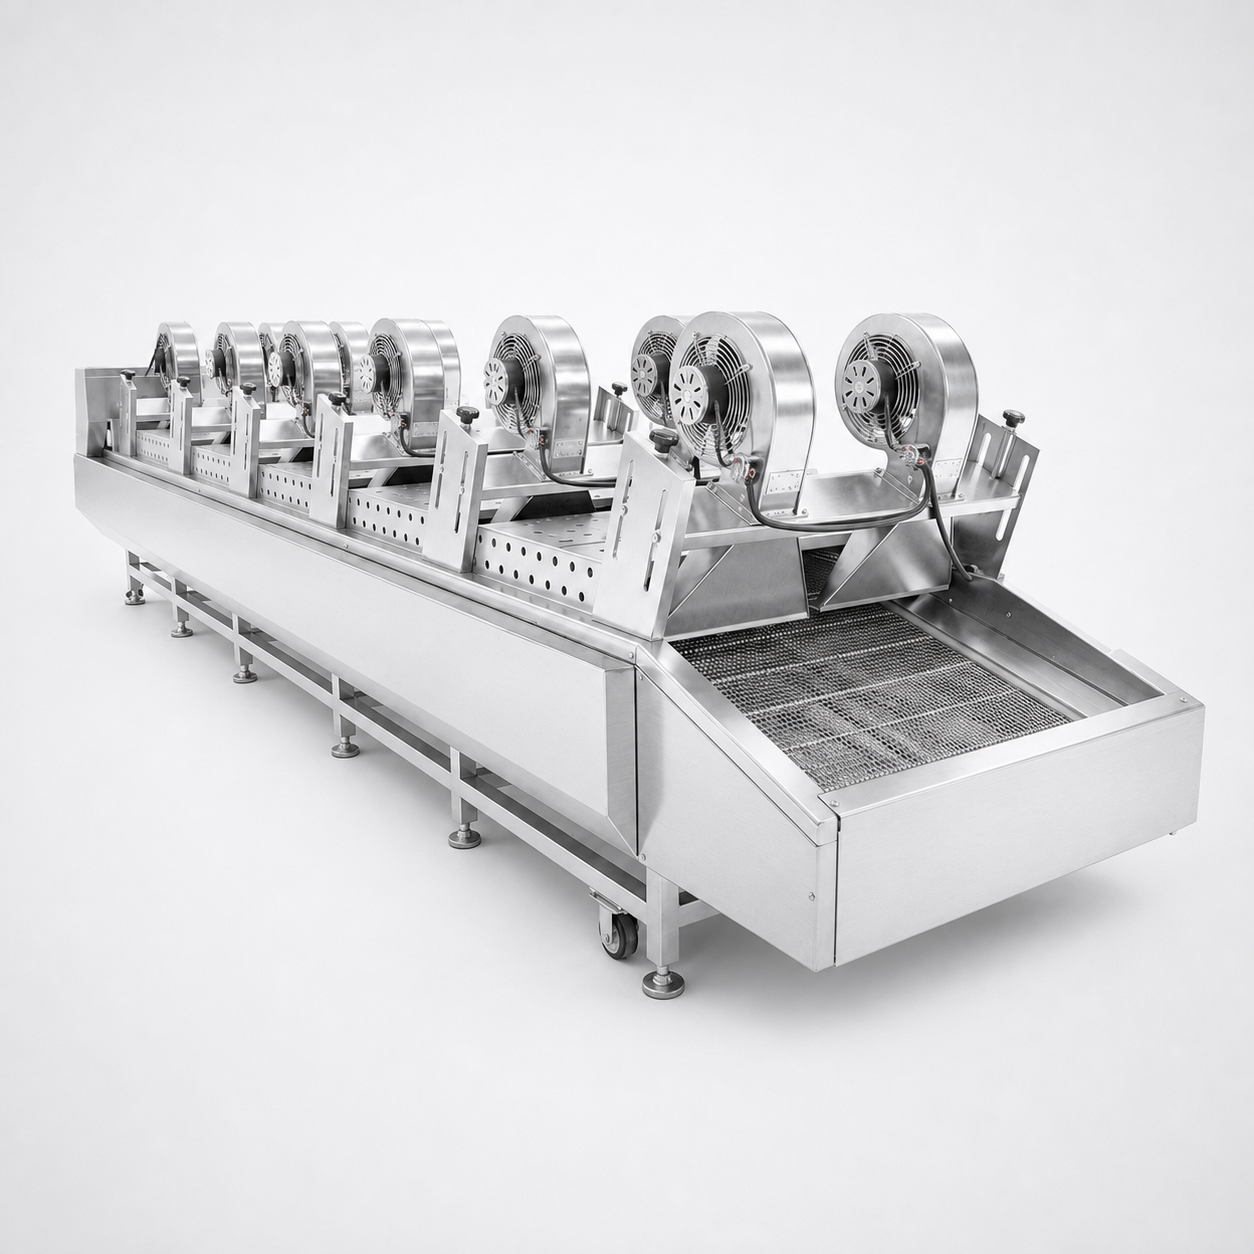
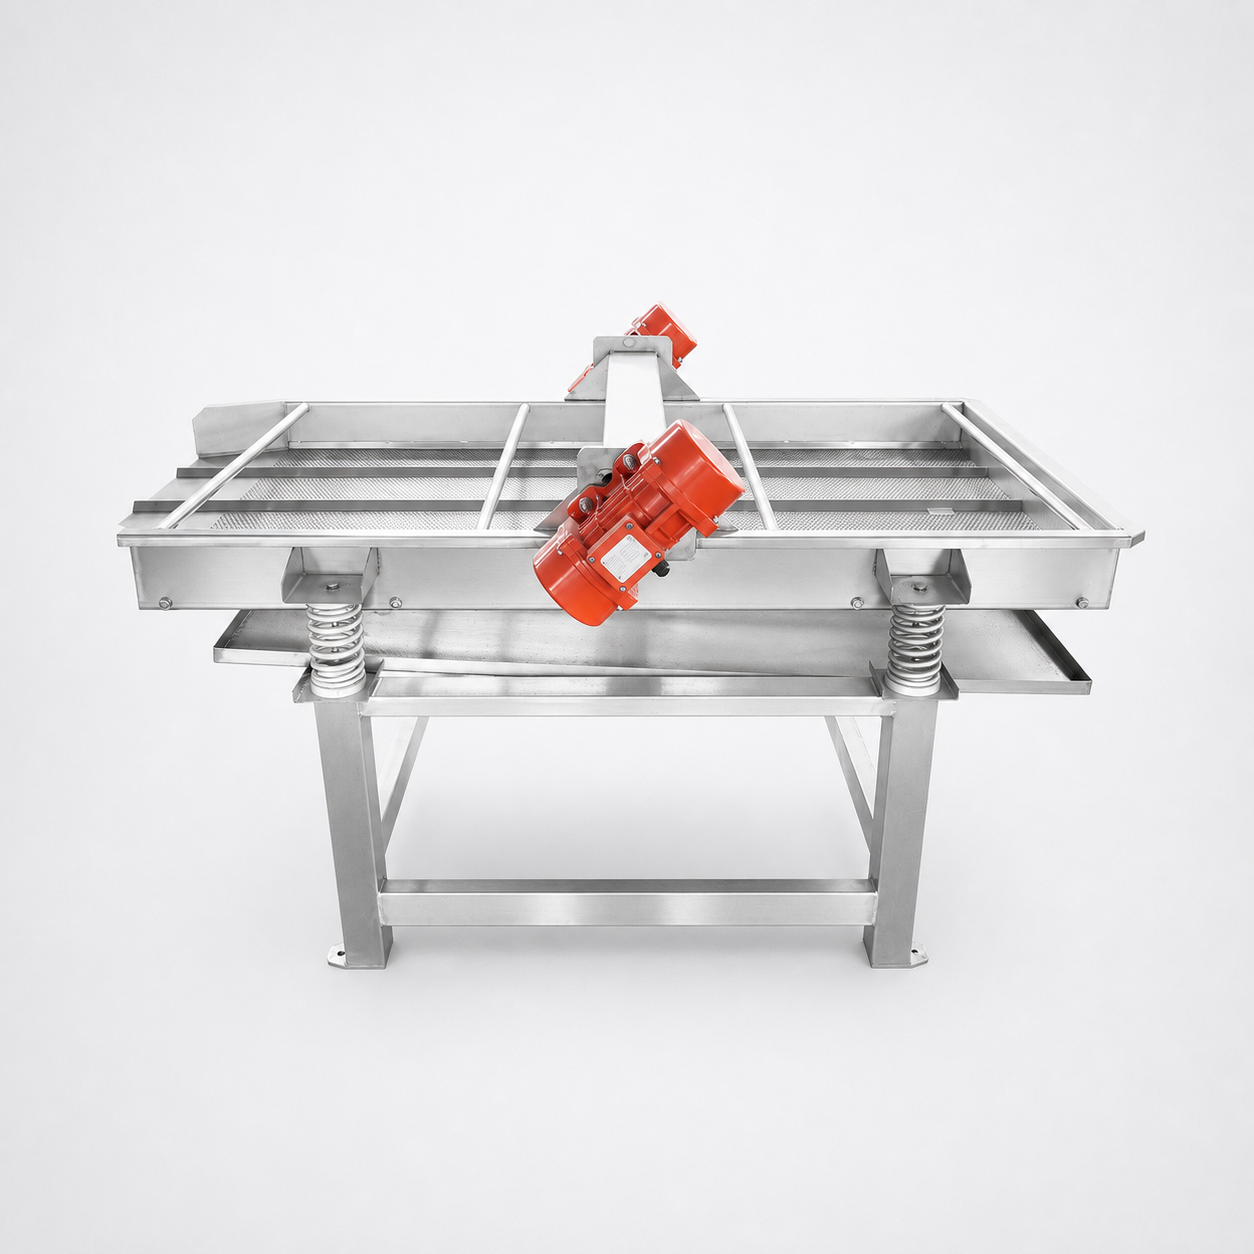
Pre-wash and soak, cutting, second wash by turbulence, third wash with sanitiser contact, vibrating dewatering, air-drying tunnel with optional centrifugal dryer, inspection conveyor, weighing and packing.
Fruit and Vegetable Dehydration Drying Line
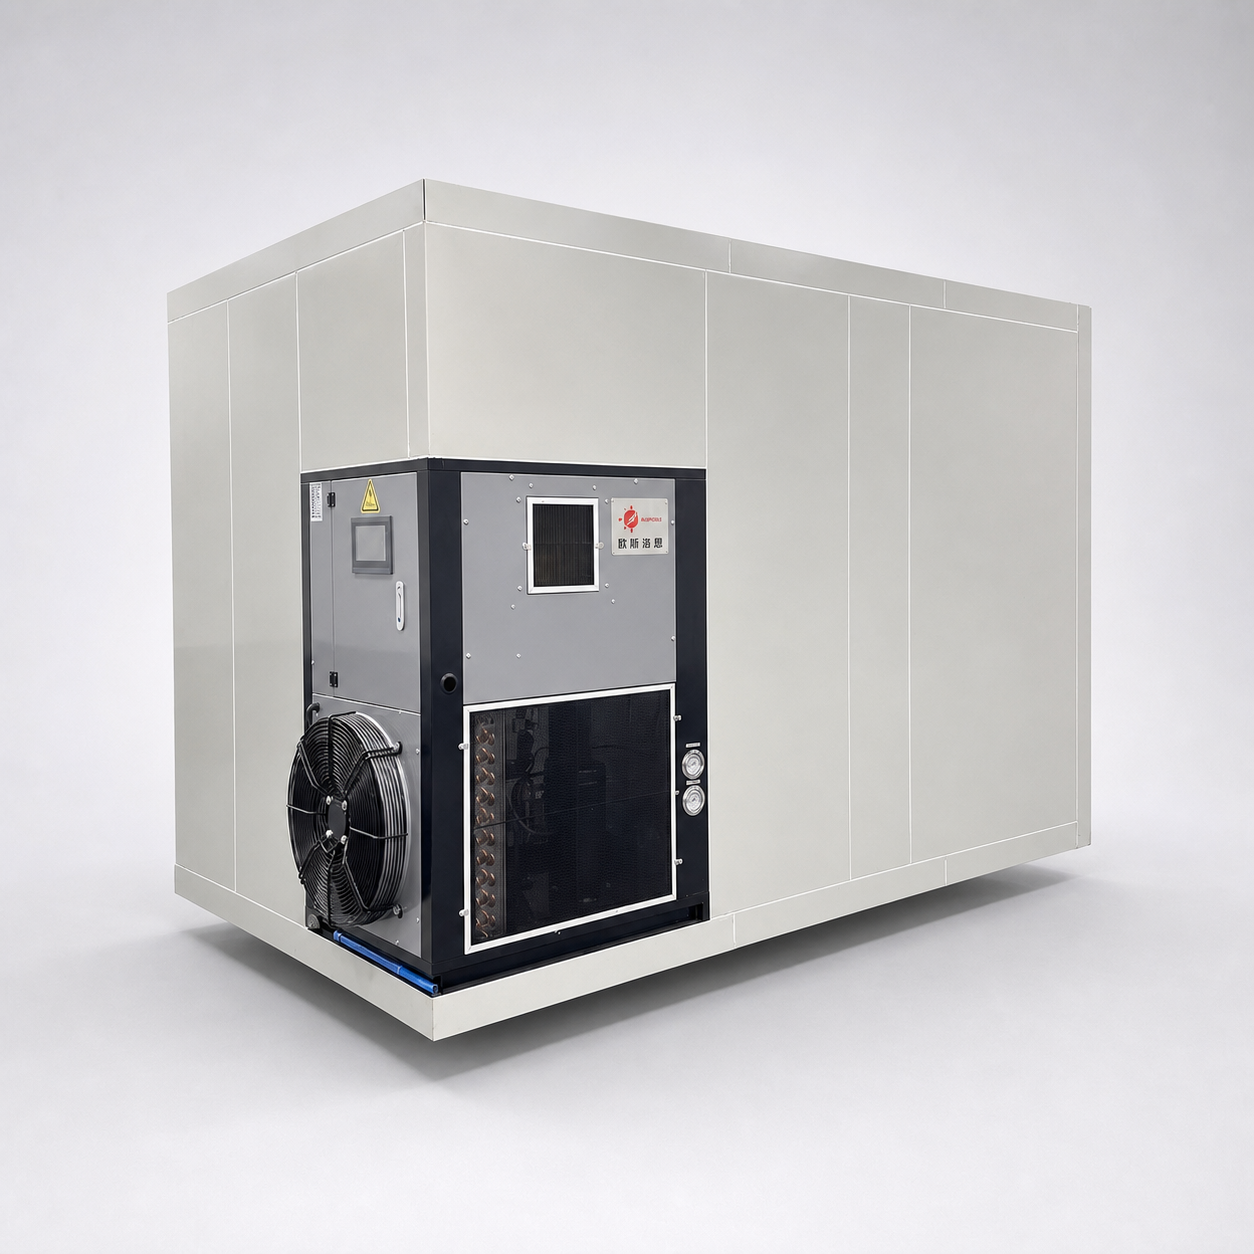
Washing, cutting and slicing, blanching, cooling, drying room, packing, with metal detection available as a station on the line.
Fruit and Vegetable Freeze-Drying Line
Wash and inspect, peel, split and trim, slice, dice or form, freeze-drying in a primary and secondary stage, unloading and packaging, metal detection.
Crops We Run Most Often
- Potato, whole washed or diced and sliced
- Carrot, whole washed or peeled into sticks and slices
- Sweet potato, cassava and taro
- Onion, ginger and lotus root
- Radish and beetroot
- Leafy greens for fresh-cut salad
- Mixed root crops sharing one line
Crop Families in Vegetable Processing and What Each One Demands
Crops do not group by botany on a processing floor; they group by what they do to the machine. Abrasion, density, skin behaviour and bruising risk are what decide the washing mechanism, the peeling method and the changeover cost. Six crop families below are how we split them.
Starchy Roots and Tubers
Representative crops
Potato, sweet potato, cassava, taro
What it demands
De-stoning ahead of the peeling machine, because field stones and grit reach the line with the crop
Line that fits
Root vegetable washing and peeling line
Throughput band
Potato 500–3,000 kg/h whole, 500–2,000 kg/h diced or sliced; cassava and sweet potato 500–2,000 kg/h
Changeover
Runs inside one family with a size setting change
Carrot, Radish and Beetroot
Representative crops
Carrot, white radish, beetroot
What it demands
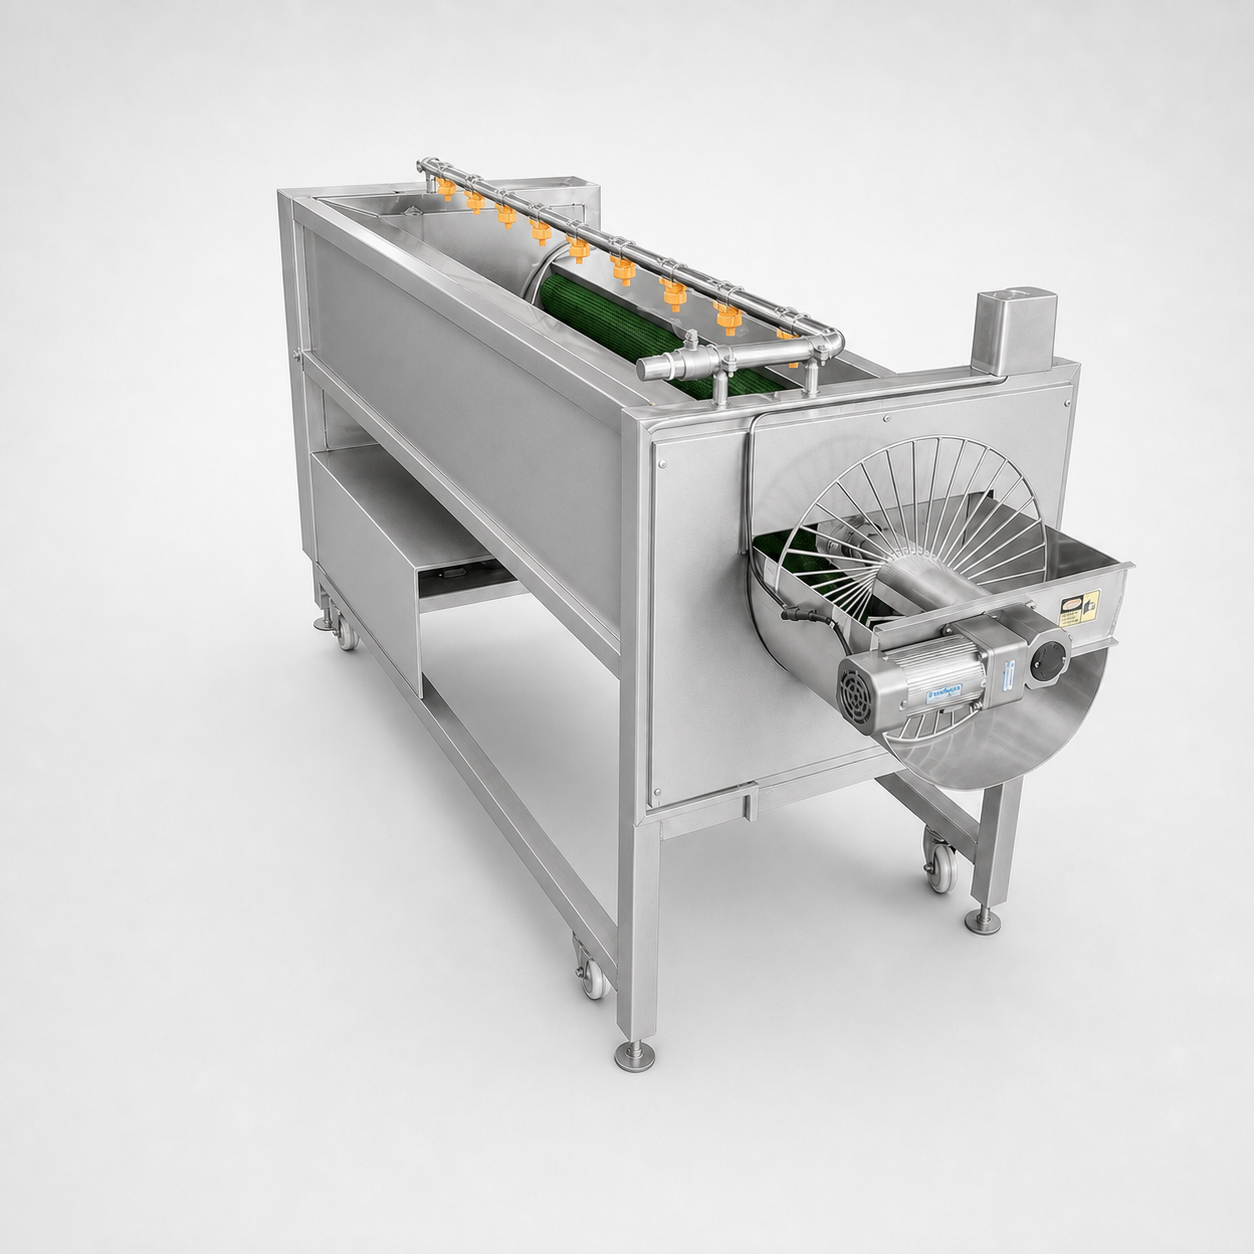
Surface-gentle washing and colour protection after cutting, since cut faces discolour before packing
Line that fits
Root vegetable washing and peeling line
Throughput band
Carrot 500–3,000 kg/h whole washed, 300–1,500 kg/h as peeled sticks or slices; radish and beetroot 300–1,500 kg/h
Changeover
Beetroot carries colour over to the next crop, so it is scheduled last in a shift or given its own run
Bulbs and Rhizomes
Representative crops
Onion, ginger, lotus root
What it demands
Irregular shape defeats uniform peeling, so these run slower and lean on sorting and manual inspection
Line that fits
Root vegetable line, or a feed section into the dehydration line
Throughput band
Onion 300–1,000 kg/h; ginger 200–800 kg/h; lotus root 200–800 kg/h
Changeover
Onion needs the line cleaned down before a mild crop follows it
Leafy Greens
Representative crops
Lettuce, cabbage, spinach and similar leaf crops
What it demands
Three washing stages and dewatering that removes water without crushing leaf structure
Line that fits
Leafy fresh-cut line
Throughput band
Built in tiers of 500, 1,000 or 2,000 kg/h
Changeover
Leaf crops share the line freely; the constraint is cold chain and shift length, not tooling
Mixed Root Crops on One Line
Representative crops
A rotating list of root and tuber crops through one installation
What it demands
The line is built around the most abrasive crop on the list, not the most common one
Line that fits
Root vegetable washing and peeling line
Throughput band
500–2,000 kg/h across the mixed schedule
Changeover
This is the family where changeover time, not machine speed, decides your real daily output, which the changeover readiness profiler works through
Fruit and Vegetables Going to a Dryer
Representative crops
Fruit and vegetable pieces destined for hot-air drying or freeze-drying
What it demands
Uniform slice geometry, because the dryer cycle is set by the thickest piece on the tray
Line that fits
Dehydration drying line, or freeze-drying line
Throughput band
Set by dryer loading and slice thickness rather than by an infeed rate
Changeover
Different products share the dryer by cycle, not by tooling
Another Crop
Send the crop, the volume you handle in a season and the form you sell it in. We will confirm which line it belongs on and what the sequence has to change before we quote anything.
Output Forms for Fruit and Vegetables: Washed, Fresh-Cut, Dehydrated, Freeze-Dried
Your product form decides the station sequence of a produce processing line more than the crop does. Adding one form to your plan adds stations, and each station is equipment, floor space and labour. Below, each form is set out with what it costs you in sequence length.
| Output form | Station sequence | Line | Stations |
|---|---|---|---|
| Washed and graded whole produce | Intake and pre-sorting, pre-wash, de-stoning, sorting and inspection, dewatering, packing | Root vegetable line, without the peeling stations | 6 |
| Peeled and cut sticks, slices or dice | Full nine-station sequence, adding peeling, cutting and post-wash with colour protection | Root vegetable line, full configuration | 9 |
| Fresh-cut leafy salad | Pre-wash and soak, cutting, turbulence wash, sanitiser-contact wash, vibrating dewatering, air-drying tunnel, inspection conveyor, weighing and packing | Leafy fresh-cut line | 8 |
| Hot-air dehydrated pieces and flakes | Washing, cutting and slicing, blanching, cooling, drying room, packing, metal detection | Dehydration drying line | 7 |
| Freeze-dried pieces | Wash and inspect, peel, split and trim, slice, dice or form, primary and secondary freeze-drying, unloading and packaging, metal detection | Freeze-drying line | 6 |
Station Sequence Explorer
All four sequences side by side, station by station, with what each station does and which stations disappear when you drop a product form.
Where a Sequence Goes Wrong
In practice the expensive mistake is settling the output form after the layout is fixed, because a station added later has to be cut into a line that already exists. Dropping dewatering from a fresh-cut sequence to save a station is the same mistake in reverse, since the salad then leaves the line wet.
Tell us the output form you sell and get a quote for the specific station sequence it needsWho Builds What
Roughly 80% of the core equipment in these lines — washing tanks, peeling machines, cutting machines, dewatering and drying sections — is built in our own plants across four cities, and the balance is sourced and integrated by us. Lines ship configured to the crop list and throughput agreed at layout approval. Nothing is added to the station sequence unless it is quoted and confirmed in writing.
Vegetable Processing Specifications
Configure your processing line throughput and analyze underlying cost drivers.
| Specification | Records to request |
|---|---|
| Potato, whole washed | 500–3,000 kg/h (1,100–6,600 lb/h) |
| Potato, diced or sliced | 500–2,000 kg/h (1,100–4,400 lb/h) |
| Carrot, whole washed | 500–3,000 kg/h (1,100–6,600 lb/h) |
| Carrot, peeled sticks or slices | 300–1,500 kg/h (660–3,300 lb/h) |
| Sweet potato | 500–2,000 kg/h (1,100–4,400 lb/h) |
| Cassava | 500–2,000 kg/h (1,100–4,400 lb/h) |
| Taro | 300–1,000 kg/h (660–2,200 lb/h) |
| Ginger | 200–800 kg/h (440–1,760 lb/h) |
| Lotus root | 200–800 kg/h (440–1,760 lb/h) |
| Radish and beetroot | 300–1,500 kg/h (660–3,300 lb/h) |
| Onion | 300–1,000 kg/h (660–2,200 lb/h) |
| Mixed root crops on one line | 500–2,000 kg/h (1,100–4,400 lb/h) |
| Leafy fresh-cut capacity tiers | 500, 1,000 or 2,000 kg/h (1,100, 2,200 or 4,400 lb/h) |
| Overall throughput envelope | 200–3,000 kg/h (440–6,600 lb/h) |
| Standard build window | 60–90 days after configuration and layout approval |
| Product-contact surfaces | Food-grade stainless steel, 304 standard, 316L on request |
Two things move a crop inside its band. Product form is the first: whole washed output sits at the top of a crop's range and peeling or cutting moves it down. Incoming crop condition is the second.
Bands describe a sustained running rate, not a peak reading taken over one minute. Washing mechanism choice itself changes the achievable rate per crop.
| Driver | Effect on cost | How to reduce it |
|---|---|---|
| Crop-family span and changeover frequency | Every extra family on the list adds tooling and takes running hours away as changeover time | Group crops by family in the schedule instead of alternating families within a shift |
| Target throughput band | Machine size at each station steps up with the band, and the step is not linear | Size for your sustained rate rather than for a seasonal peak you run a few weeks a year |
| Output form, which fixes the station count | Nine stations cost more than six, in equipment, floor space and operators alike | Confirm the product form you actually sell before layout, and add stations later |
| Contact-surface material grade | 304 is standard and 316L is a specified upgrade, priced where it is applied | Apply 316L where your product and cleaning chemistry require it |
| Depth of automation and digital integration | Low-code control boxes, multi-protocol gateways, machine-vision inspection are separate scope | Start with control and data collection, and stage vision inspection into a later phase |
| Drying route energy intensity | Freeze-drying and hot-air dehydration are not in the same class for energy or capital intensity | Match the route to the product value |
Holding Cost, Published
145–165%
Five-year total cost of ownership of initial equipment.
3–6%
Annual maintenance of equipment cost.
2–4%
Annual spares of equipment cost.
Lowest bid is rarely the lowest total price. Payback depends on your crop value, utilisation and labour rates.
How Your Quote Is Produced
- 01. Send your crop list, target kg/h and output form.
- 02. Our team reviews the inputs to propose a line route and confirms the quotation timing for your project.
- 03. Configuration approved, written quotation follows.
| Order stage | Lead time |
|---|---|
| Layout & Config | Runs until layout approval |
| Production | 60–90 days post-approval |
| Shipment | Stated in quotation |
Contact Surfaces, Metal Detection and Food Safety Checks
Food safety on a processing line is decided at three points: what the product touches, what gets caught before packing, and who looks at the product in between. Each of the three is a design decision, not an inspection afterthought. Here is how each one is handled.
- Food-grade stainless steel, 304 as standard, 316L on request where product chemistry or cleaning regime calls for it.
- Carbon steel is excluded from the food-contact zone.
- Finish grade is fixed at configuration against your product, not assumed.
- 3-A Sanitary Standards Inc, the standard-setting body, writes that the standard maximum surface roughness for product-contact surfaces is often set at 32 micro-inch (0.8 micron) Ra, and attributes that figure to its own standards, USDA guidelines and EHEDG. It also states in the same publication that for many applications the traditional 32 micro-inch standard may be adequate for safe production, balancing product, operating conditions and cleaning practices. That qualification matters as much as the number: the issuing body treats it as an application-dependent starting specification, not as a cleanability guarantee.
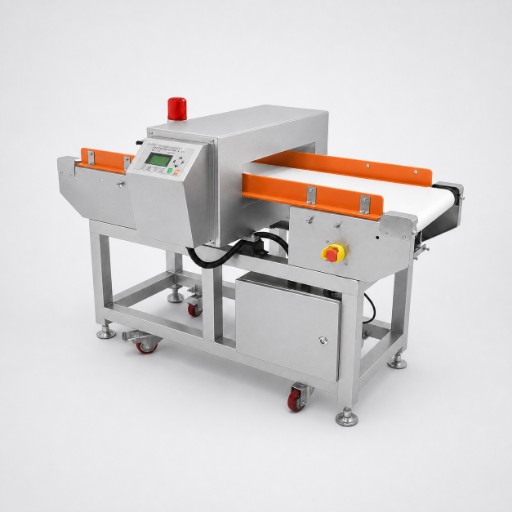
Metal detection as the final station of the freeze-drying line
- Freeze-drying line: metal detection is the final station of the six-station sequence.
- Dehydration drying line: metal detection is available as a station on the line after packing.
- Root vegetable and leafy lines: the standard sequences end at packing and at weighing and packing. If you need metal detection on either, raise it at configuration so it is in the layout rather than retrofitted.
- Intake and pre-sorting removes undersize, damaged and foreign material before it can reach a machine.
- De-stoning takes out field stone and grit ahead of the peeling machine, protecting both the equipment and the product quality downstream.
- Sorting and inspection sits mid-line on the root vegetable sequence, and an inspection conveyor sits immediately before weighing and packing on the leafy line.
- Metal detection closes the freeze-drying sequence, after packaging rather than before it.
- For a fresh-cut leafy operation, the reference document your quality team will map the line against is the US Food and Drug Administration's guidance for industry on minimising microbial food safety hazards in fresh-cut fruits and vegetables. Our leafy line is built with three separate washing stages, so that mapping has three points to work against.
Vegetable Processing Equipment Built in Our Own Plants
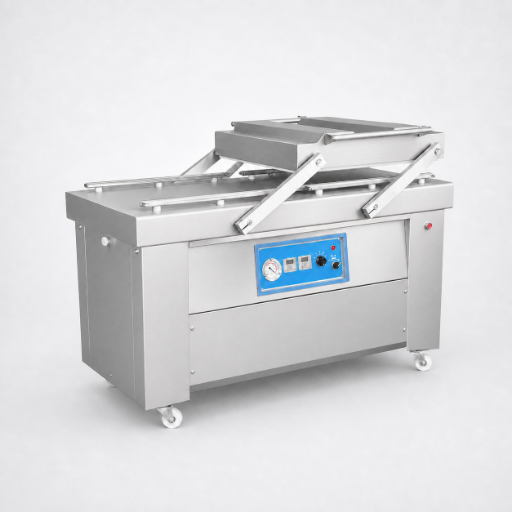
Our four owned and self-built manufacturing bases cover approximately 80% of our main equipment categories. Specialized or supplementary equipment is supplied by long-term partner factories. Our headquarters are in Zhucheng, with branches in Qingdao, Changzhou and Weifang; the company has more than 20,000 m² of office and display space across these cities, including an approximately 5,000 m² food machinery showroom.
What Sits Behind the Machines
The company that builds the line also writes the control software for it. That is why a line can ship with low-code control boxes, multi-protocol gateways and standalone over-the-air upgrades instead of a third party's controller bolted on afterwards.
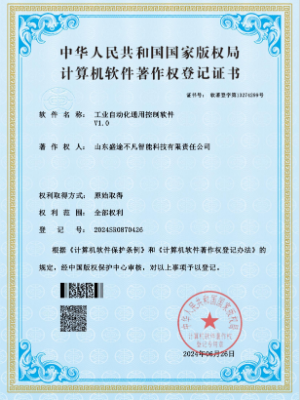
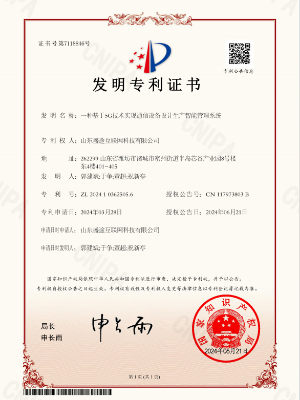
- More than 100 registered software copyrights and 7 patents sit behind that software, developed across more than 100 R&D projects.
- The STUnit platform carries the machine vision, edge algorithms and gateway functions, and it is ours rather than licensed.
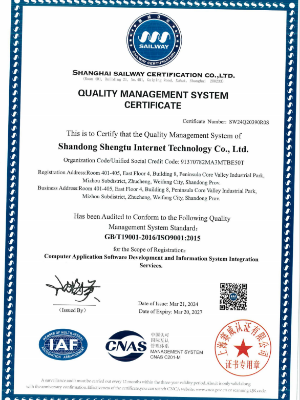
- Request company management-system, assessment and recognition records relevant to the proposed supply. Confirm each record's holder, scope and current status.
Read that last line narrowly, because it is worth less than it looks. A management-system certificate says a company runs documented processes; it is not a performance rating for your line, not a food-safety approval, and not an acceptance certificate for your project. Ask every supplier on your shortlist for line-level evidence separately, ourselves included.
Processors We Build For
Root Vegetable Packers
Whole washed and peeled-and-cut output on a nine-station line, 200–3,000 kg/h depending on crop.
Fresh-Cut Salad Processors
Eight-station leafy lines built at 500, 1,000 or 2,000 kg/h, with three washing stages and air-drying.
Dried Fruit and Vegetable Producers
Seven-station hot-air lines with blanching, cooling and a drying room ahead of packing.
Freeze-Dried Snack and Ingredient Makers
Six-station lines running primary and secondary freeze-drying and closing with metal detection.
How We Work: From Configuration to Handover
You send three things — the crop list, the target kg/h and the product form you sell. That is enough for us to route you.
Design Notes That Lower Your Cost
| Design decision | What to specify | Why it saves money |
|---|---|---|
| Crop list | The crops you will actually run in year one, with the seasonal share of each | A line built for a crop you run three weeks a year carries that cost for its whole life |
| Throughput | Sustained kg/h at the product form you sell, not the peak hour | Machine size steps at each station, so one band down can remove a step across several machines |
| Station sequence | The output form now, with the space reserved for stations you may add | Reserving floor space is cheap; rebuilding a layout to insert a station is not |
| Material grade | Where 316L is genuinely needed rather than line-wide | That upgrade is priced where it is applied, so targeting it keeps the rest at 304 |
What to Check Before You Commit
Check whether the manufacturer still supports the model you are buying and whether spare parts stay obtainable, and put that question to every supplier on your shortlist, including us. Our answer is that roughly 80% of the core equipment in these lines is built in our own plants, so parts for those stations come from the people who made them. Ask for the parts list at configuration rather than after commissioning.
Get a Line Proposal
ENGINEERING TOOLS
Engineering and Planning Tools
Frequently Asked Questions
What is a fruit and vegetable processing line?
A connected sequence of machines that takes raw produce from intake to packed product, each station doing one job and passing the crop to the next. You buy the sequence, not any single machine.
Can one line handle both fruits and vegetables?
Within a crop family, yes — our root vegetable line runs a mixed root schedule at 500–2,000 kg/h. Across families the honest answer is that it depends on abrasion and shape: de-stoning and brush peeling built for cassava are wrong for soft fruit. Tell us the full crop list and we will say which parts share a line and which need their own.
How do I choose between washing, fresh-cut, dehydration and freeze-drying?
Answer three questions in order: which crops you run, what throughput you need in kg/h, and what form the finished product leaves in. Those three route you to one of our four lines, and the grid near the top of this page shows the routing. Crop decides the mechanism, because abrasive roots and soft fruit pull the contact surfaces in opposite directions. Throughput decides the size of each station more than it decides how many stations there are. Product form is the one that changes the sequence outright: washed and packed ends at dewatering, fresh-cut adds cutting and spin-drying, and dehydration and freeze-drying each add a dryer plus the handling around it. If two of the three are already fixed by your business, the third is usually a commercial decision rather than a technical one.
What is the production capacity of your lines?
Our envelope is 200–3,000 kg/h, and the rate depends on the crop and the product form. Potato runs 500–3,000 kg/h whole washed and 500–2,000 kg/h diced or sliced; ginger and lotus root run 200–800 kg/h; leafy lines are built in tiers of 500, 1,000 or 2,000 kg/h. A full per-crop table sits in the throughput section above.
What materials are the machines made of?
Product-contact surfaces are food-grade stainless steel, 304 as standard and 316L on request. Carbon steel is excluded from the food-contact zone. A published benchmark for contact-surface roughness is 32 micro-inch (0.8 micron) Ra, from 3-A Sanitary Standards Inc, and the finish grade is fixed at configuration against your product.
Are your washing machines water-efficient?
Water use is a property of the washing mechanism rather than of the brand: air bubble, vortex, brush-and-spray and drum pre-wash differ in water consumption, bruising risk and how they handle stone and sediment. A percentage saving quoted without the crop, the mechanism and the configuration behind it is not something you can budget against. The washing mechanism selector walks through the choice crop by crop, and all four are compared on the root vegetable line page. Soil load matters as much as the machine: a crop arriving with field stone needs a pre-wash stage ahead of the main washer, and leaving it out moves the cost into water rather than removing it. Which mechanism suits your crop is the right question, because that is what sets your water bill.
Can your machines be integrated into an existing line?
Yes. We build with low-code control boxes and multi-protocol gateways so a new section can talk to equipment already on your floor, and upgrades can be delivered over the air to a standalone machine. Send the layout of the line you already run and we will do a fit check against it before anything is quoted.
Do you provide customized solutions?
Every line we ship is configured rather than picked from a shelf: the crop list sets the washing and peeling method, the product form sets the station count, and the throughput sets machine size at each station. Our customization happens inside four standard sequences of 9, 8, 7 and 6 stations. That keeps delivery predictable while still fitting the plant to your crop.
How long is the lead time?
Production runs are scheduled at 60–90 days after configuration and layout approval. That window covers manufacture and assembly; it does not include sea freight or site work, and it does not start at first enquiry. The configuration stage ahead of it runs at your pace, which is why we ask for the crop list and target kg/h up front.
What are your payment terms?
30% deposit and 70% before shipment by T/T. Terms are confirmed in the quotation together with the configuration they apply to. We do not publish a price list, because a price without a configuration is noise.
Are you a direct manufacturer?
Yes. Four owned and self-built manufacturing bases cover approximately 80% of our main equipment categories; specialized or supplementary equipment comes from long-term partner factories. Our four-city office and display footprint exceeds 20,000 m², including an approximately 5,000 m² food machinery showroom. The manufacturing source and integration responsibilities are confirmed in the quotation.
Can we still get spare parts and support years after installation?
Ask this of every supplier you shortlist, because parts access for imported equipment is where buyers most often get caught. Roughly 80% of the core equipment in these lines is built in our own plants, so the parts for those stations come from the people who made them. The remaining stations are the ones worth pinning down in writing: ask which are bought in, from whom, and what the lead time on a replacement looks like once the original maker revises the model. Ask for the parts list at configuration rather than after commissioning, and upgrades to a standalone machine can be delivered over the air.
How do the machines reduce labour cost?
Labour comes out of the stations that are otherwise manual: sorting, peeling, dewatering and packing. Automatic conveying also removes the handling steps between those stations, which is where a lot of hidden labour sits. We do not publish a percentage saving, because it depends on your crop, your current line and your shift pattern rather than on the equipment alone.